
Injecting pressure switch and water-confined motor logic
Release time:2026-09-20
Use the short-shot product weight and watering to close the test to determine the switch point the pressure pressure and the time of the pressure. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
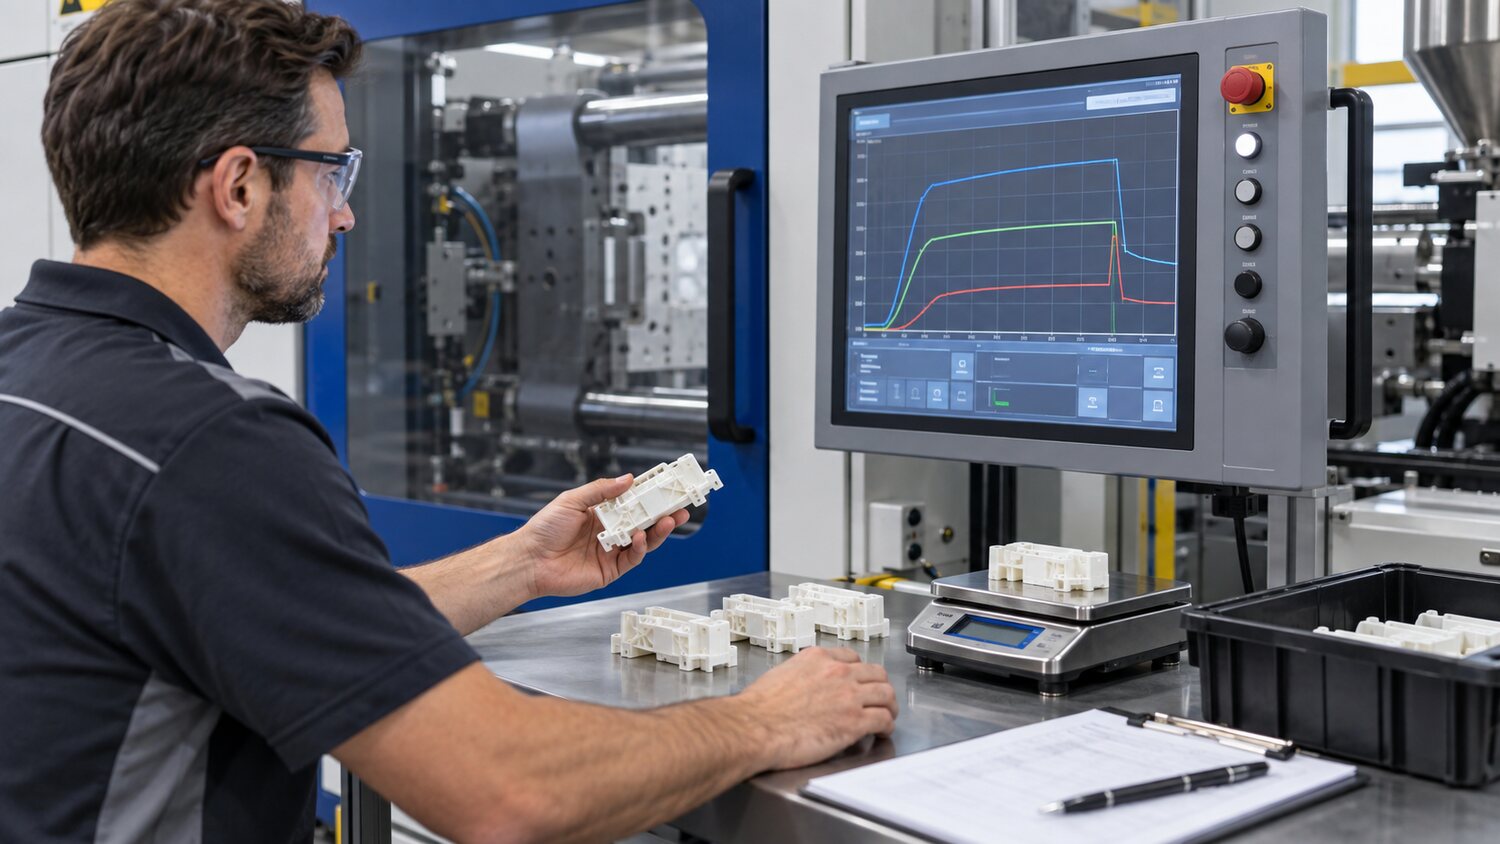
Switching from velocity control to pressure control is a key node for determining product weight, flying edge, water loss and size stability. In the case of premature transitions, the cavities are not fully filled, and the pressure will have to cover work that should have been done at injection speeds, which can easily result in short-shot, visible melting and weight fluctuations; in the case of late transitions, the molten has already pressed the cavities and the equipment is still advancing in a velocity mode, and is susceptible to pressure peaks, flying edges, internal stresses and overloading. Switching can be done by lowering the pressure, confirming the level of filling by short-shot, and by placing the switch points at approximately 90 to 98 per cent of the product. The scale is to be verified on the basis of product rigidity, type of watering, platform response and material compression and cannot be mechanically applied.
Once the switch point has been determined, the moderate pressure pressure is established and then the pressure step test is performed. The other conditions are maintained, with a gradual extension of the pressure time at fixed intervals, with each condition being described as a continuous product. When the mass of the product increases over time into the platform area, it means that the watering is closed and that continued pressure will only increase energy consumption and cycles and will no longer be able to send the molten body into the mold. The time of effective protection should be slightly covered by the watering of the closed points, with attention to size, constriction and demolition stress. Heavy-watered, thick-walled items usually require long-term pressure protection; needles or thin-walled blocks are sealed faster and, if they are still under long pressure, they often create excessive pressure and bleaching near the watering.
The pressure's not as high as possible. The higher voltage compensates for the cooling of materials, but also increases residual stress, top loads and stylings, and the transparency element may have a risk of stress break. A more rational approach would be to use a sub-push: the previous paragraph would be used to stabilize the recharge, the middle paragraph would be reduced by the gradual freezing of the spill and the last paragraph would only maintain the necessary pressure. The weight and critical dimensions of the product should be monitored for shell sizes that are high; if the weight is stable and the sizes fluctuate, the problem may come from the temperature, waterways, cooling imbalance, fibre orientation or demodelization, rather than from continued increased pressure.
Switching stability is also affected by the cessation of retroring seals, mats and measuring duplication. At the end of each module, a reasonable mat shall be retained so that the screws do not end; in the case of a material cushion that is too small, is not consistent with the pressure curve or changes in the cyclicality of the product ' s weight, a check shall be made for the reversal of the ring ' s wear and tear, the spiral ' s reflow, nozzles and plasticization measures. In the case of multiple cavities, if there is a significant difference in the size of the different types of cavities and the total pressure cannot be increased to force compensation, the fluid balance, mouth size and exhaust should be checked first. A good switch should keep the pressure curve smooth, produce weight stable and leave room for material viscosity changes.