
How to control the filling quality at the speed of the segment.
Release time:2026-09-20
Set speeds between thick structures and the end of the flow, balancing the appearance of size with the exhaust of the mold. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
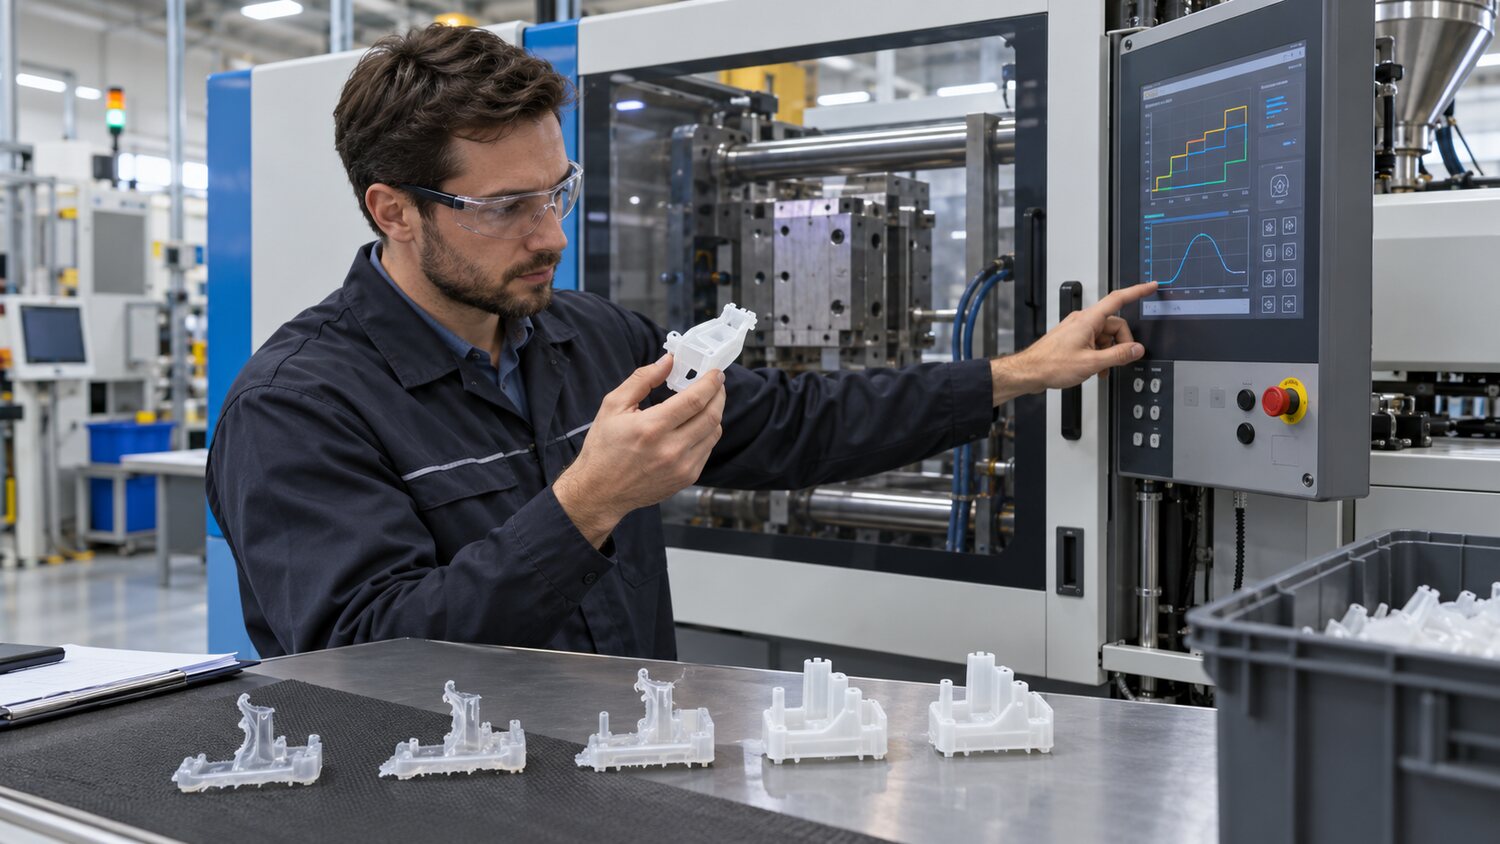
Injection speed determines the manner in which the front line of the melting is advanced and also directly influences the cutting of heat, flow marks, melting lines, congested air and fibre orientation. The switchboard cannot be understood as the faster, the easier to fill, nor can it be used at one speed from the nozzle to the end. A more reliable method is to combine the position of the screw or the injection volume classification phase: the molten is to be stabilized through the nozzle and the main channel; to control the cut in accordance with the size of the watering; to increase the speed of large thin-wall areas, as appropriate, in order to avoid early freezing; and to reduce the speed close to the end of the vent, the plate or the small column, allowing time for air discharge. Each segment should be located at a moving boundary of short-shot samples, rather than being filled in at will with experience.
High-speed fillings have the advantage of reducing front temperature, reducing flow marks and increasing the replicability of thin walls, but at high speed they can cause spray threads, burning, flying edges, albinization and breathing. Low speed can reduce inertia and cut, but can result in cold threads, visible melting lines, surface fog or underfilling. Therefore, the velocity is to observe both actual injection time, peak pressure and pressure curves. If the actual injection time following the increase in the set speed is not shortened and the pressure is close to the ceiling for equipment or molds, indicating that the process is constrained by the pressure, the continued increase in the set speed does not lead to a real high speed, but rather conceals the problem of too low flowways, low ventilation or low temperature.
For products with multiple sips, long processes or visible thin changes, the screw position corresponding to each structural turning point can be determined by short shot. For example, if the melting is just past the vent, it accelerates when entering the main surface, slows back through thin ribs or at the far end, and retains a stable reduction period until the pressure is replaced. Transparents, mirrors and high-light Electro-shells are all the more important to avoid a lull in the front line, as mutations of flow speed leave light and pressure marks. Probate boosters also control overcuting to prevent excessive fibrous fractures or the formation of a clear orientation in the vicinity of the vent, which changes the direction of the arcs with their speed.
The velocity programme shall be subject to a fixed temperature, back pressure, pressure and cooling condition, adjusted for only one velocity or one switching position at a time, and at least a number of continuous models shall be observed. The eligibility criteria are not only physical but also a comparison of the weight of the product, the strength of the melting line, the critical dimensions and the end-stage exhaust. If a deficiency can only be eliminated at an extreme speed, the ability to water, fluid, exhaust and screw plasticize should be further examined, as speed compensation tends to shift the problem to flyside, residual stress or equipment load. Ultimately, each location and the corresponding product structure should be included in the parameters, so that the next switchman knows the reasons behind the setting, rather than copying only a string of numbers.