
Note system check and modeling methods before plastics go on.
Release time:2026-09-20
The establishment of a matrix in four respects of the material Modified Equipment and Process Benchmark to reduce the recurrence of parameters as soon as they are activated. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
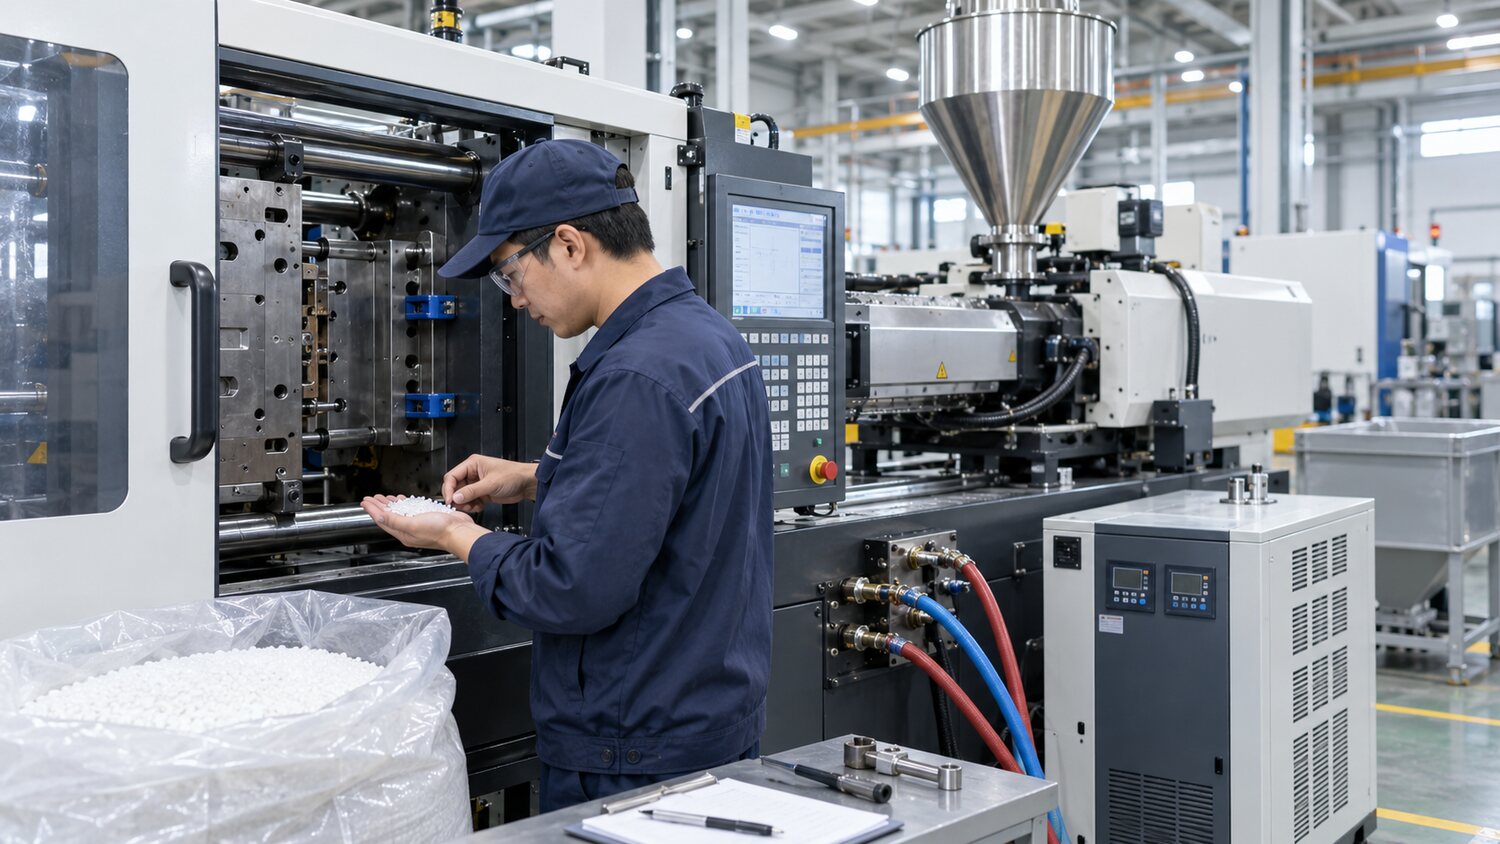
The first step of the pyrotechnics is not to increase pressure or heat immediately, but to confirm that production conditions are renewable. The material plate number, batch, chromosomal ratio, repost ratio and dry record should be checked prior to start-up to confirm that there are no residues from the previous order in the casket, pipeline and magnetic shelf. For humid materials, the dry temperature, time and spot are determined on the basis of the material supplier ' s technical data table; the internal moisture is not judged to be satisfactory by the mere fact that the particle surface looks dry. In the case of moulds, check whether the waterway is aligned, whether the flow is normal, whether the temperature in the hot-flow zone is stable, and whether the top and core movements are smooth, and confirm that the vents, watering mouths and substrates are not blocked by oil or residual glue.
The focus of the equipment inspection included the temperature control of the material drums, thermal electromechanicals, retroring, nozzle co-operation, screw position sensors and lock-molecular protection. When setting the temperature, do not produce immediately, and should allow sufficient equal temperature time for the drums and thermal currents, then use low-speed plasticization to observe whether the current, back pressure and measured time are stable. It is recommended that the pressure be removed or lowered, that short-shot tests be conducted at lower injection speeds, that the amount of gel be gradually increased, and that the actual flow order of the melting be confirmed from the vent to the end. This allows for the identification of problems of filling imbalances, air, cooling and watering freezes and avoids overstretching of mold defects.
In the establishment of the matrix, the temperature, temperature, screw velocity and back pressure of the drum shall be fixed and filled with injection velocity and switching position control. When filled to about 90 to 98%, switch to the pressure, and then water the closed point through a gradual increase in the pressure time judgement; when the pressure time continues to be extended and the weight of the product does not increase, the pressure time is shown to be close to the effective limit. The cooling time should be based on the product being stabilized, critical dimensions not to continue to drift and do not undergo white transformations, rather than simply pursuing the shortest cycle. Each time only one major parameter is changed and the weight of the product, peak pressure, measurement time and cycle are recorded, it is possible to know which adjustment actually works.
In the case of long-term dissimilar convulsive time fluctuations, black dots, unmelted particles, or reductive endpoints, it is not possible to continue to increase temperature and pressure only on the screen, but also to check the match between the diameter of the screw and the amount of the voltage, the suitability of the screw compression and measurement segments for the current resin, the return of the reversible ring and the wear of the screw and the drum. The reasonable goal is not to make a decent sample, but to establish a process window with a residual amount of small fluctuations in material batches, ambient temperature and equipment. Once the header model is confirmed, the version of the parameter should be preserved, along with the retention, mass and critical size criteria, as a uniform basis for subsequent shifts and repeats.