
The repulsive screw turns to plastic stability.
Release time:2026-09-20
Understand the co-effects of back pressure and screw velocity on mixing exhaust temperature rise and measuring repetition. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
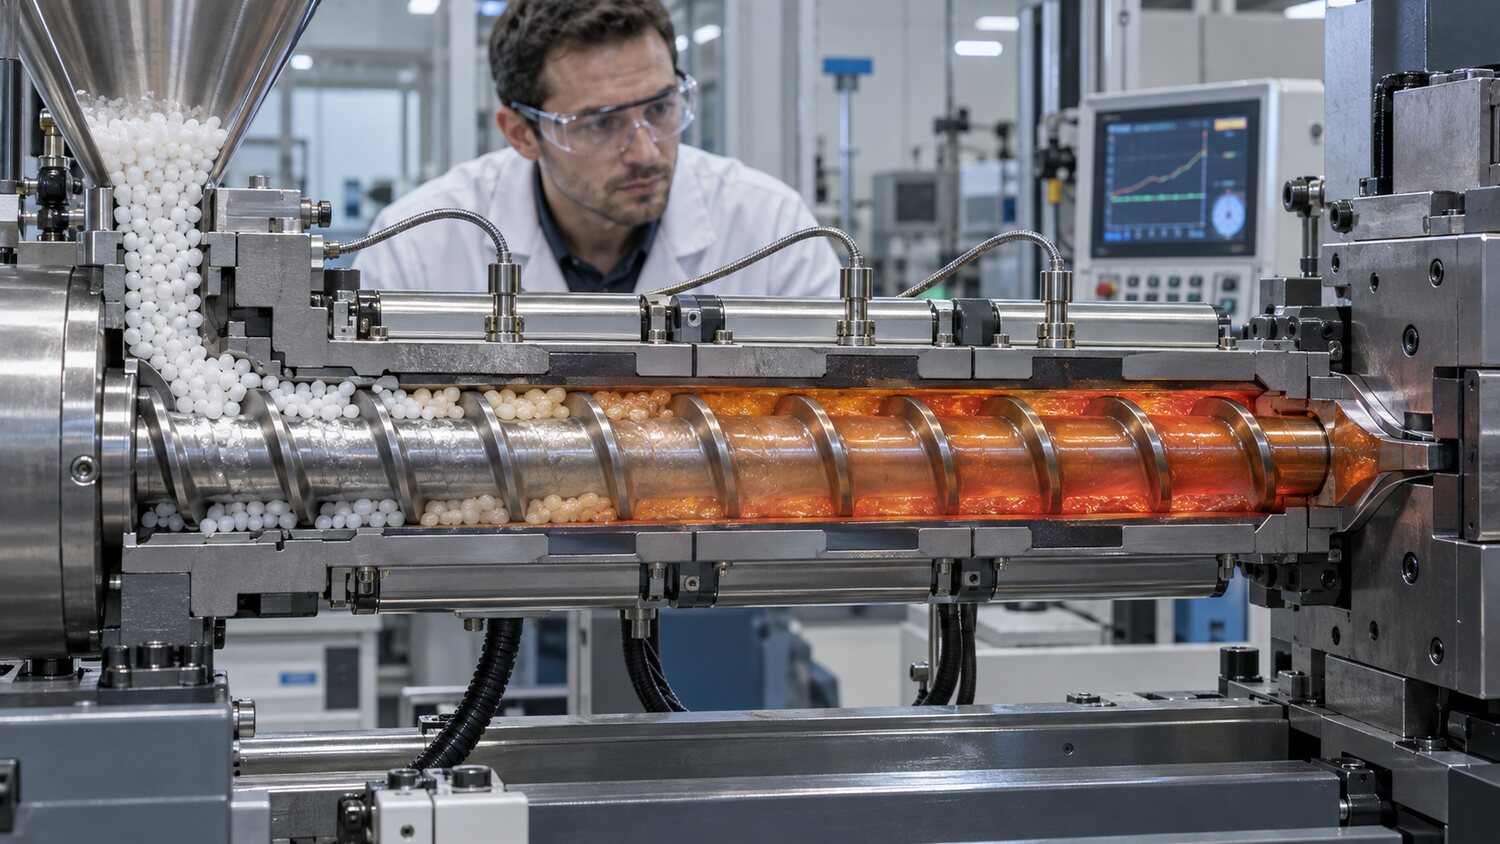
The back pressure and screw velocity determine the delivery, pressure, melting and mixing mass of the particles in the drum. When the back pressure is too low, it may be accompanied by more air, with an uneven distribution of color mothers and a high degree of volatility in the measurement of density and product weight; excessive back pressure increases the plasticization time, increases the shearing heat and energy consumption, changes the heat-sensitive material, overcuts the fibers and accelerates the wear of the screws and drums. The correct approach begins with meeting the minimum back pressure of plasticizing evenly and measuring stability, observing whether the smelting looks, measuring time, and the spiral retreats are smooth, then adjusting to product requirements in small amounts, rather than using high back pressure as a solution to all the mixed problems.
The spiral speed determines the number of cuttings and the rate of heat production within the unit time. Low rotation speeds can help to reduce material overheating and fibrous damage, but if plasticization is not completed during the cooling phase, it may prolong the cycle or result in a shortage of the next simulator feed; while a shorter measurement time may result in a significantly higher actual melting temperature than that set for the drum. The switchboard should contain the plasticization time within the cooling time and retain a certain amount of spare time to avoid the application of glue as soon as the screw is measured. For PC, POM, PMMA, fuel retardants and botilizers, special attention should be paid to cutting temperature rises, odours, colour changes and nozzle saliva.
Measuring travel also affects the quality of plasticization. The application of too little and too large screws in diameter, the material's actual replacement rate in the drums is low, its duration is long, and it is easy to produce black dots, yellow transformations and decomposition; it is too large and may require a long measurement process, which leads to a lack of supplies or an uneven melting process. In the case of long-term unmelted particles, colour differentials, measured time fluctuations or overheavy temperatures under the same parameter, a check should be made as to whether the screw diameter, long-range ratio, compression ratio and condensed structure match resins and products. Increasing the back temperature or back pressure alone may temporarily improve the appearance, but may reduce the safety process window.
When plasticizing parameters are established, measurement time, screw endpoints, peak twists or currents, product weights and actual cycles can be recorded for a continuous period of 20 or more. If the measurement time is extended over time, it is necessary to check the fillings, the plume, the cooling water is too strong, the screws slide, or the material contains water; if the measurement suddenly becomes faster and is accompanied by a decrease in weight, it is suspected of stopping the reverse loop flow or changes in the particle density. A stable plasticization process should achieve even melting, moderate mixing and recalcitrant measurement, while avoiding unnecessary high shearing, which is the part where material and capacity assessments are most needed to select and customize the plastic screws.