
How do we fix the note? Reason, process, mold and screw optimization
Release time:2025-10-02
How do you address the causes, processes, molds and screw optimization of the note? The wall thickness and reinforcement position should be checked first, and the pressure, cooling and melting measures should be adjusted for stability; increasing pressure without examining the mold and plastic state is often difficult to stabilize. This paper combines information on star-friend screw stations to organize selection, process and validation elements.
Core conclusions of the Note Speculation Solutions
The wall thickness and reinforcement position should be checked first, and the pressure, cooling and melting measures should be adjusted for stability; increasing pressure without examining the mold and plastic state is often difficult to stabilize.
Note Shrink Solutions
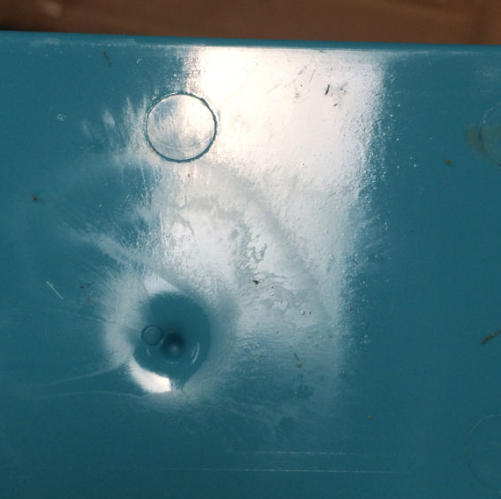
Shrimp marks are surface defects of the plating plastics due to uneven cooling contractions, most of which occur in wall thickness and spasms, which affect the appearance and structural stability of the product and require a combination of process adjustments, model optimization and screw optimization.
1. Core characteristics
(b) A local dent in the surface of the product (deep 0.1-0.5 mm), in a circular, elliptical or irregular form, with a sense of dent in touch;
Most commonly around wall-heavy transition areas, sprawl roots and BOSS pillars;
More evident in transparent / light colour products, even in dark colour products, can affect surface flatness.
2. Main causes
(b) Inappropriate pressure: insufficient or too short pressure pressure, and non-melting during cooling contraction;
(b) Too high the temperature of the molds: slow cooling, leading to over-scaling;
Crystal material characteristics: A high rate of crystallization (3-5 per cent) of crystallized materials such as PBT, PA (polyamide) and not compensated through the process;
Poor plasticization of screws: Normal screws are unequally plasticized to material, and the density of the molten body fluctuates, leading to poor constriction consistency.
Practical solutions
Optimizing the safety parameters: Adjusting the pressure pressure to the wall thickness (60-90 per cent of the injection pressure), extending the time of the pressure (from 5 seconds to 10-15 seconds) to ensure that the smelting space is adequately replenished;
(a) Control of the temperature of the mould: setting the temperature of the mould on the basis of the characteristics of the material (PBT 50-70°C, PA66 40-60°C) and encrypting cooling waterways in the thick wall area;
(a) Spiral optimization: Gradivate compression relative to the screw (compression ratio 3.5-4.5), extension of the measurement period (25-30% of the total length of the screw), polishing of the screw surface to Ra 0.1-0.2 and coating of CrN (chromium nitrogenization);
Modular adjustment: Set a condensed truncheon (radio 0.5-1.5 mm) at the root of the band, reduce the local thick wall to 3-4 mm and add a reinforced band to ensure structural strength.
Data to be recorded before implementation
- Material integrity number, filling ratio, flame-retarding system, refill ratio and dry condition.
- Note plastics brand, model, screw diameter, voltage, back pressure, turn speed and current screw structure.
- Indicators of product size, wall thickness, appearance or strength, and current adverse phenomena and frequency of occurrence.
- Continuous production cycle, refuelling frequency, machine clean-up method, wear and tear record and planned useful life.
How to validate the adjustment results
It is recommended that the current process baseline be established, followed by a single-variant test model. Each round records the measurement of time, melting temperature, product weight, formation cycle and bad rate, avoiding multiple parameters being changed at the same time to determine the cause. The parameters in the text are used to illustrate design thinking and should not replace material supplier data and on-site safety protocols.
What kind of support is a star-friend screw?
The Starfleet Mechanical Equipment Co. Ltd. in Dongqing City (Starfung) can provide a reset of material and work evaluation, screw structure recommendations, base and surface treatment options, non-spectrometric customization, and trial modelling issues around the abbreviated plastic coding solution. The submission of information on raw materials, equipment and products could lead to more targeted programmes.
Ask for customized screws immediately, or check firstNote plastic screw productwithNote Plastic SolutionsI don't know.