
Balancing modems and abnormalities for the heat flow molds
Release time:2026-09-20
Thermal routing methods are built around heat-steal temperature differentials, cavity balance, watering state and material time. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
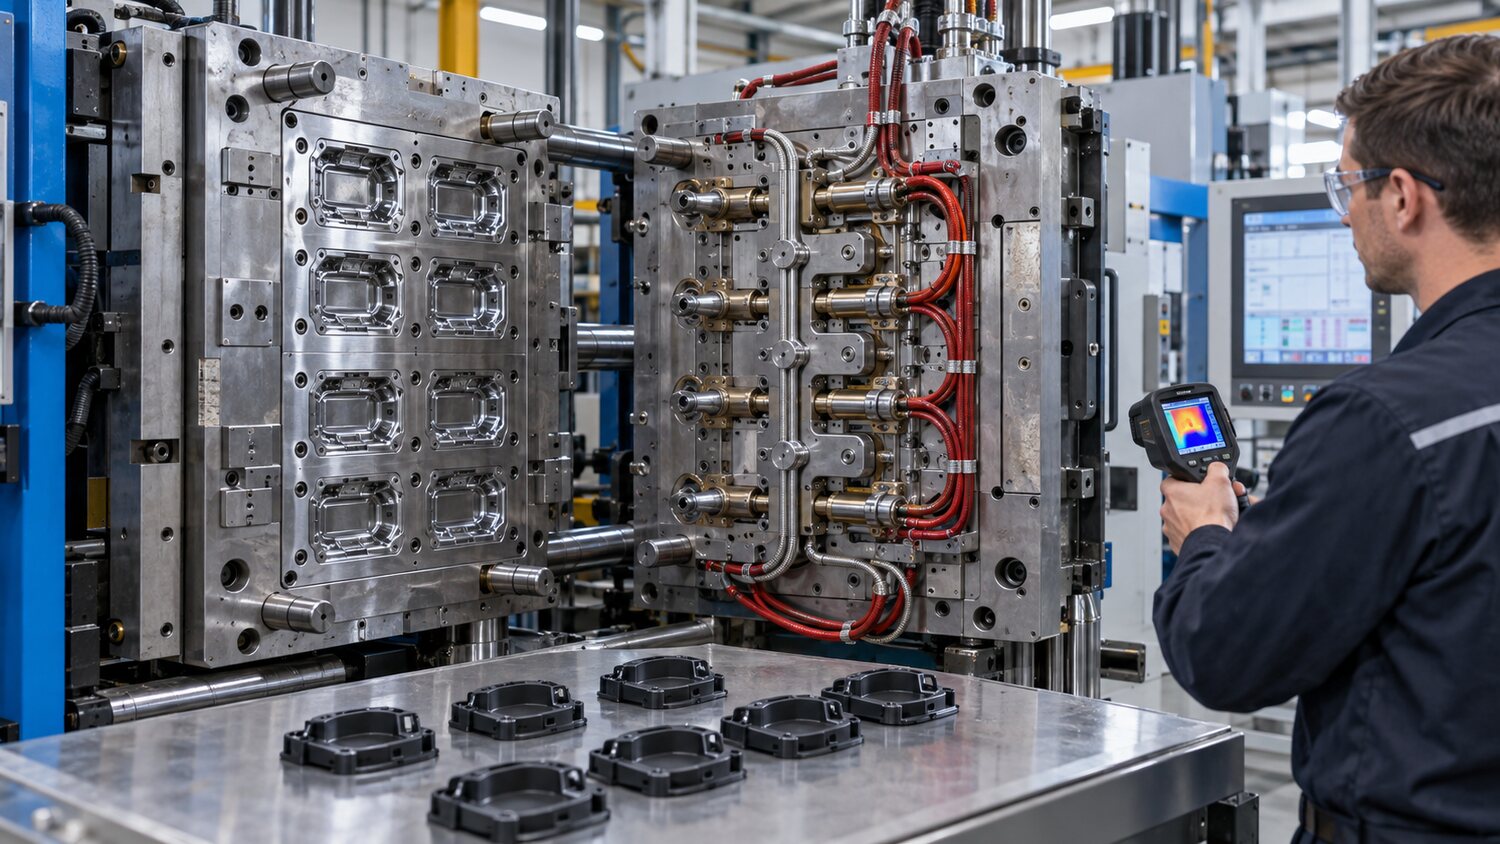
Thermal currents reduce cooling and watering waste, but there are more meltings stored in the system, which are more sensitive to temperature homogeneity, retention time and flow balance. It should be opened in the order of the supplier of the mold, confirming that the actual temperature in the temperature areas is stable and then slow-temperatured, and avoiding the partial non-melting of high-pressure gel damage valves or heat sticks. The thermostat displays the same does not mean that the heat-bracket export state is consistent, and the position of the thermal electromechanical doll, the heating ring exposure and the tip of the mouth spread causes real differences. Multi-cavette moulds should be recorded separately for each cavity weight and filling order, and the balance of the system cannot be judged by the total weight alone.
In the event of a cavity short-shot, fly-side or colour anomaly, a determination is made as to whether the problem is fixed in the same heat. Fixed single cavity abnormalities are usually associated with heat-barrel temperature, squeezing, valve travel, flow size or local exhaust; if abnormally randomly moved, they are more likely to be related to the measurement, reversal, material moisture or overall process fluctuations. The temperature of the thermal stench should be adjusted in small steps and for time to stabilize, and excessive temperature increases the risk of rassing, salivation, mouth glitter, material decomposition and color differentials, although this can temporarily reduce viscosity.
The sequence valve heat flow also controls the opening of the valve. Late start-up may result in visible melting marks or pressure waves, with early start-up and possible reversals, flow marks and local overpush. In combination with short-shot samples and pressure curves, the melting line should be determined when it reaches each vent, and the opening of the valve sequence optimized. For large exteriors, the melting line position can be controlled by a valve sequence, but the temperature of the thermal stench and the response must be consistent, otherwise the defects will drift after the change of batch. The pressure phase should also identify which water can still be effectively filled and should not be used for the same time.
Cut-off and color change are high-risk links in the production of thermal stream. There are branches and dead corners within the system and it is difficult for colours or materials to be cleansed at once; prolonged high-temperature waiting leads to carbonization of residues and continuous black spots. Temperature, clean-up and re-heating procedures should be developed based on the compatibility of resins, using the appropriate clean-up material where necessary and avoiding direct propulsion of incompatible materials into the system. If black dots and colour differences persist, the dead end of the heat stream, the pointy carbon of the mouth and the screwdriver mix should be checked, rather than indefinitely prolonged cleaning. Stable thermal stream production relies on co-comparisons of temperature control, valves, plasticization and the exhaust of molds.