
High-speed accelerator advice for food packaging thin wall products
Release time:2026-09-20
Optimizing the high-speed filling of the cavity balance and short-cycle stability for thin wallglass boxes, lids and food packaging. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
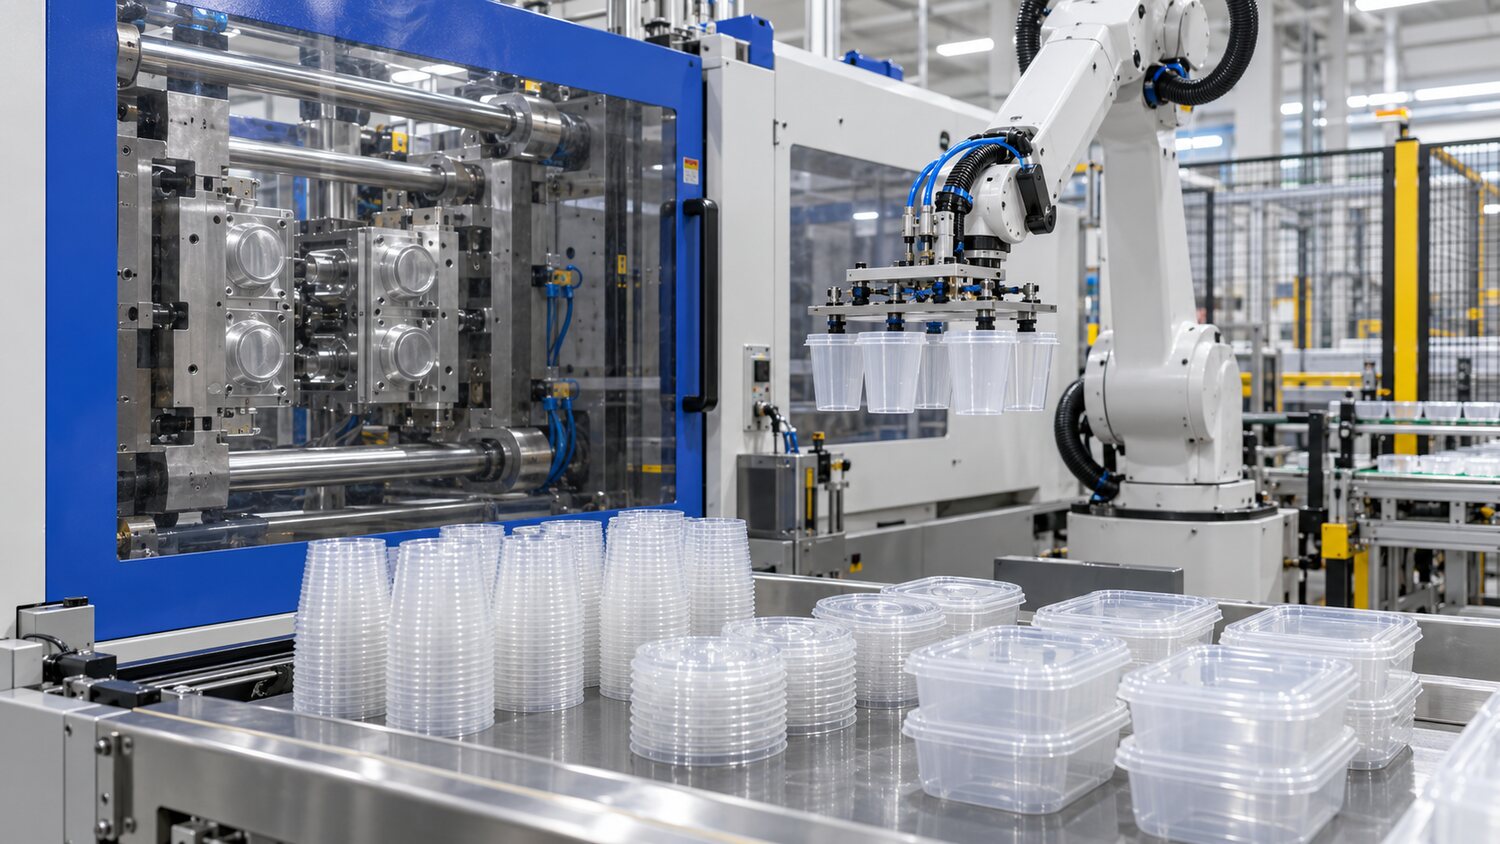
Food-packing thin wall products are more often used as food-exposure-level PP or PE or may use materials such as transparent PS. The product walls are small, long, long, long and short-cycle, with the goal of rapidly filling and maintaining the same weight per cavity, while meeting the requirements of falling, stacking, sealing and food exposure. Raw materials, colour mothers, demodulants and retrofitants must be in compliance with project regulations and customer norms and should not increase uncertainty at will to reduce costs. Particle Melting Rates must be matched with equipment injection speed and screw plasticization capability.
Threads require a higher actual injection speed, not just a high set value. The actual injection time and pressure curve should be viewed to confirm that the equipment did not lose speed control due to the pressure ceiling. Short-shot samples are used to check the synchronity of the various types of cavities and, in the case of a cavity or long-term short-shot at the far end, the flow, heat, mouth and exhaust balance should be handled instead of increasing the overall pressure to make the near-end cavity fly side. At the end of the filling, moderate deceleration can be achieved to reduce the convulsions, burns and stymied shocks. The speed pressure switch must be stable to prevent instant overloading of the mold.
The time of the pressure is usually subject to a rapid closure of a small sip, which should be determined through a weight platform test and should not be customarily long. The cup mouths, lids and button sizes require sufficient pressure, but excessive pressure can cause difficulties, stress and periodic waste. The cooling time shall be combined with mechanical manual pick-up, stacking temperature and product deformation verification; a thin sheet that appears to be normal and may continue to deform under automatic stacking pressure. The stability of waterways, thermal fluids and the temperature of the cavity surface directly determines the reliability of high-speed continuous production.
Short-term cycles require the screw to complete stable plasticization within cooling time. It also accelerates wear and tear if the propeller is in a very high state for a long period of time, when the measurements are applied immediately after the end, and the temperature of the molten and the chromosomal rises. Snails with sufficient plastic capacity, appropriate diameter and refining capabilities should be selected and time trends measured. The mass is produced with a record of each cavity weight, cycle, peak pressure and bad position, and a temperature differential or reversal is detected in a timely manner. Food packaging products are ultimately certified by stacking, sealing, falling, odour and regulatory requirements, and not only unit cycles as the only objective of optimization.