
Home Electro-High-Purpose Emulator Proposal
Release time:2026-09-20
Accommodation of the flow marks of the large exterior of ABS and PC ABS Melting wire Water shrink colour differences and assembly transformations. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
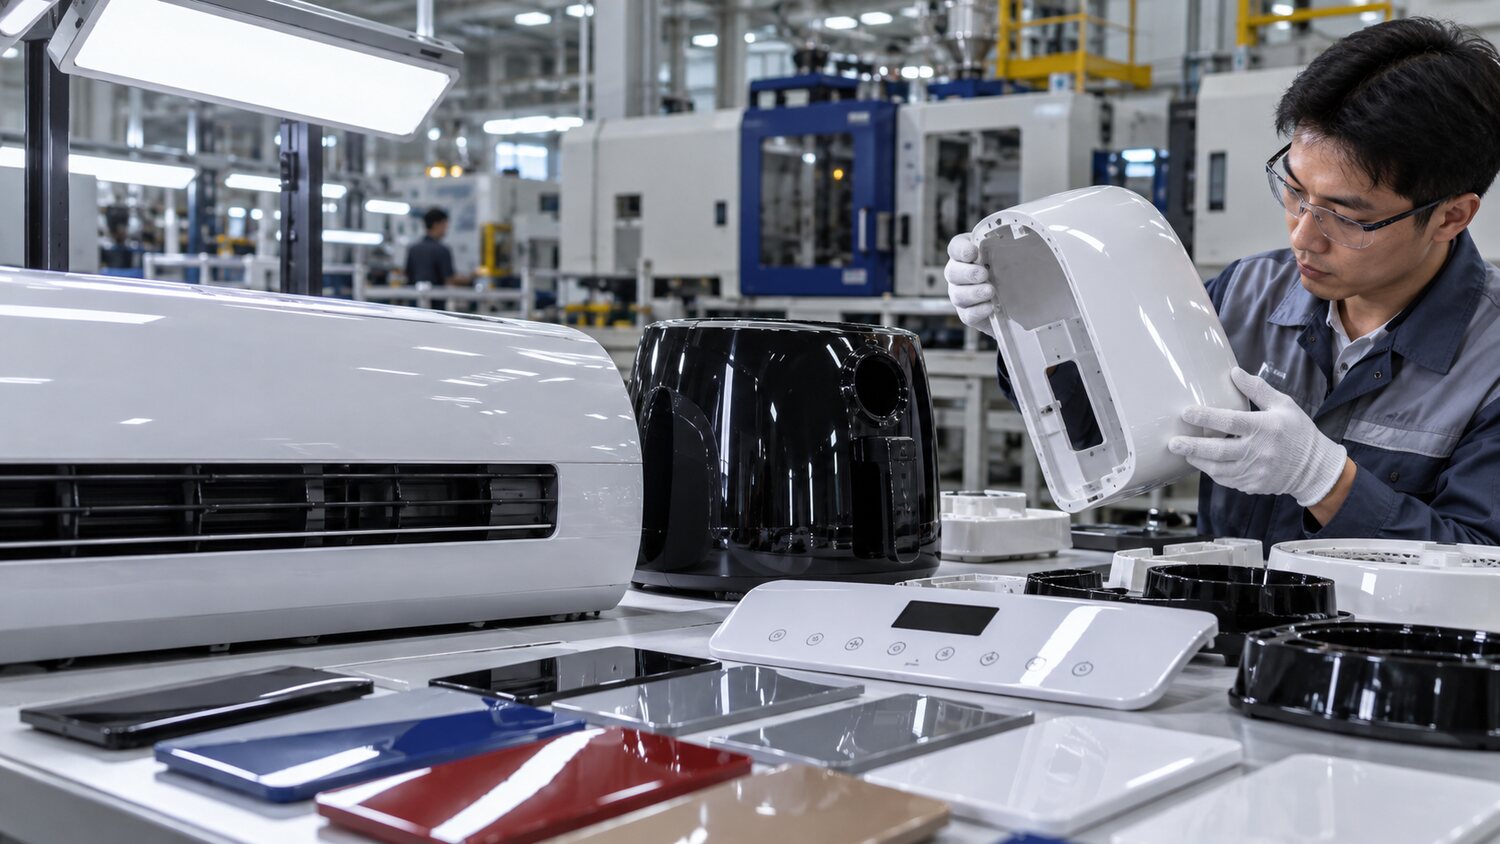
The ABS, PC ABS, HIPS or modified PPs are often used in television frames, air conditioners panels, small household electric casings and control panels. Such products are large and continuous in size, with flow marks, melting wires, water shrinkage, white and colour differentials that can be easily detected, while ensuring a gap between bolts, brakes and assembly. The switchboard shall be preceded by a confirmation of the drying of the material, the colored parent ratio, the texture of the mold and the cleanness of the high light, and shall specify the requirements for subsequent spraying, wiring, welding or electroplating. The tolerance of residual stress and surface pollution varies from post-process to process.
High light surfaces usually require high and even temperatures, stabilization of the melting line and sufficient vents. Shortshots can be used to identify the melting position in the main exterior and to set the speed of the segment to avoid sudden changes in the speed of the flow. High-speed watering and thin-walled areas produce spray marks or bleaching, and the end is too fast and charred. In the case of improved melting lines at very high temperatures, both material stopovers and colour changes should be checked, particularly flame retarding ABS and PC ABS.
Bands and bolts shrink from structure, pressure and cooling. When watering can be effective in filling, the dents can be reduced by reasonable switching and sub-push; if the watering is frozen or too thin, continued pressure can only generate flight edges and internal stress. The large-area panel arc should compare the aerometric temperature, local waterways and peak timing. Mechanical handbanding and stacking can also deform products that have not been fully cooled, so cooling times are subject to physical automation.
Black dots and colour differentials of high-light products are often associated with the dead end of the screw, thermal flow of carbon, the dispersion of chromosomal mothers and the retention of materials. Colours shall be changed using compatible machine clean-up procedures and the examination of nozzles, reversible rings and screwheads. If a shell is filled for a product or mineral, the mills are also considered for grinding and fibre orientation. The Quantification Standards shall include specification of the appearance, mass of products, critical assembly dimensions and post-process tests under the light source. The stabilization process should be able to remain eligible for small changes in material batches and ambient temperature, rather than relying on a shift-by-class of aircrews to follow the defective modifications.