
Electronic Connector and Precision Plugin Emulator Recommendations
Release time:2026-09-20
For the thin wall end of the trough, small needle feet and fiber-fibre flame retardant material, control the lack of glue, burn the edges and dimensions. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
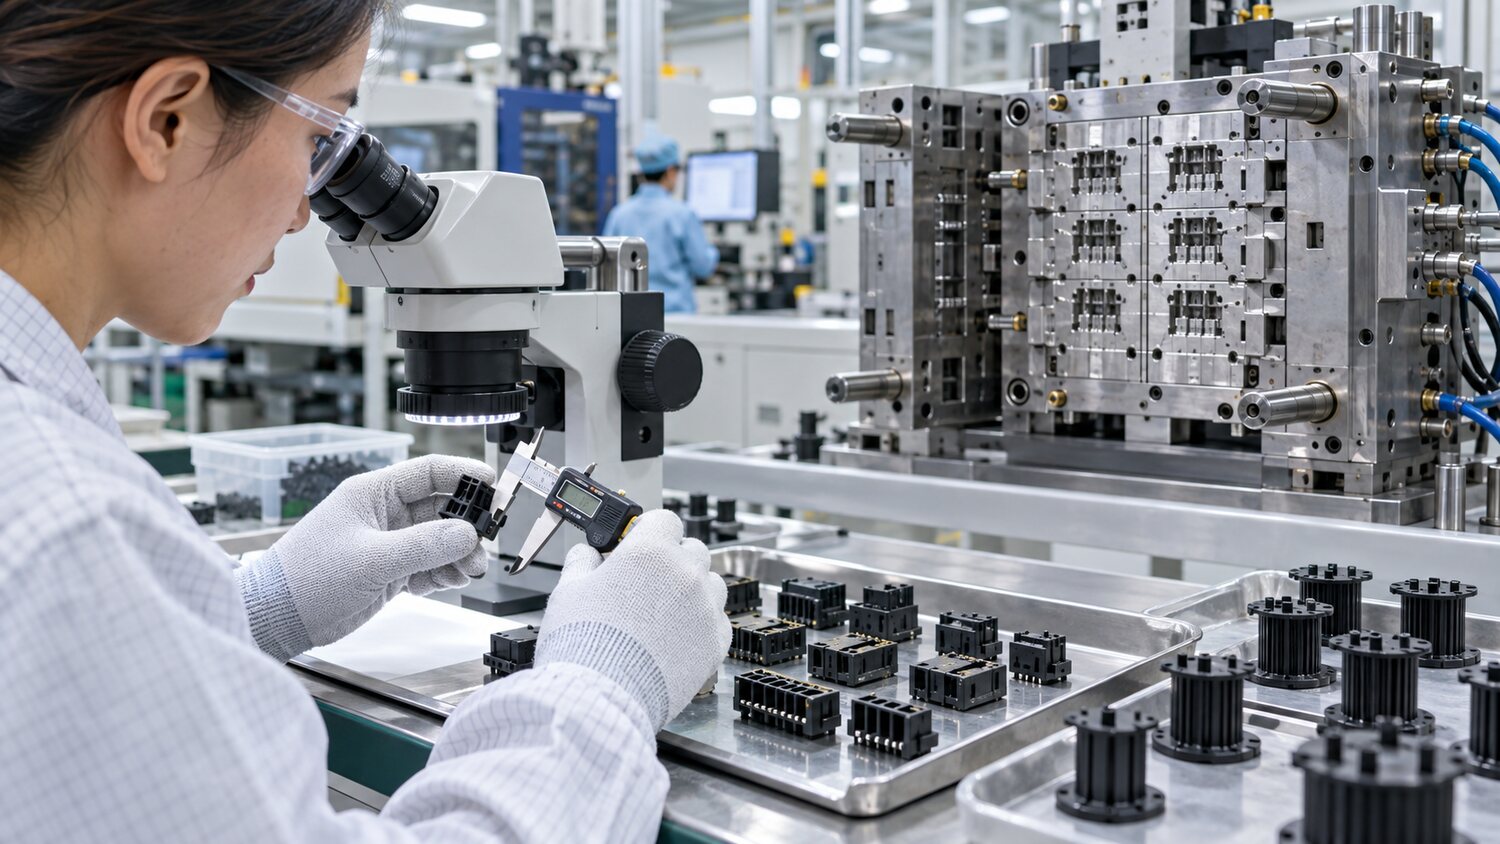
Electronic connectors, coil skeletons and precision plug-ins typically use boron to enhance PA, PBT, LCP or other flame retardant engineering plastics. The product is small, but is thin, thick, and contours are dense, requiring high demand for venting, modulation, material moisture and anti-reversity stability. The transfer is preceded by a confirmation of the drying record of the material, the flame retardation grade, the percentage of the fiber and the proportion of the allowed retrospect, and a check of the embedded or endpoint positioning. In the case of oil, water or hair puncture on the endside surface, which can cause damage to the combination, gas stripes and molds, all defects cannot be attributed to gel pressure.
A short-shot-based segment velocity is recommended for filling. Meltings need to be fast enough to enter the main area of the thin-watered mouth and the thin wall to avoid the cutting-edge freeze resulting in a lack of foot; they should slow down at the end of the foot of the needle, at the end of the blind and at the end of the current, and allow time for air to eject. The combination of burning and lack of glue is often a distressing signal, at which point the continued increase in speed and pressure will only worsen. The vents, pins and collages are regularly cleaned because of the ease with which pelicans, flame retardants and volatilizers form sediments. Multi-cavette moulds should also be rated per cavity product, confirming flow and thermal stench balances.
hairside control cannot be based solely on increased locking power. Spills are generated by late switching, over-pressures, wear and tear of the moulds, stifling of the ends or a decrease in the material ' s actual viscosity. A short-shot should be used to determine the switch point, with the starting point for the minimum effective pressure to meet the size and strength. For end-pack rubber, an over-melt impact may drive or bend the end of the end, and the stress can be reduced by changing the direction of the injecting, the front speed and the ender fixation. Shorter cooling can deform a tiny structure at top, and the size test should specify the time of placement.
Fossil flame retardants accelerate the wear of screws, drums and reversible rings and are sensitive to the time of stay. Small low-yielding products are prone to changes in black dots and colours if they are over-used with large drums and materials are slowly updated. Suitable screw diameter, grinding material and non-removable angle structure should be selected, with back pressure and turn speed based on full plasticization and non-overcution. Connector mass production cannot only look, but also verify end position, pull, voltage resistance, size and melting line strength. Process windows should have clear upper and lower limits for moisture, pressure curves and per cavity weight.