
How the new plating project creates a screwdriver selection needs table
Release time:2026-09-22
For the project manager of the Apostille Processor, describe the method of checking the product size, single weight, wall thickness and energy target, analyse the risk that incomplete information will lead to a disconnection between the screwdriver programme and the actual work situation, and provide recommendations for the validation of the construction of the product, raw material, platform, molds, a table of needs in the five columns of the process and the trial period, the time of plasticization, and the mass stability of the product.
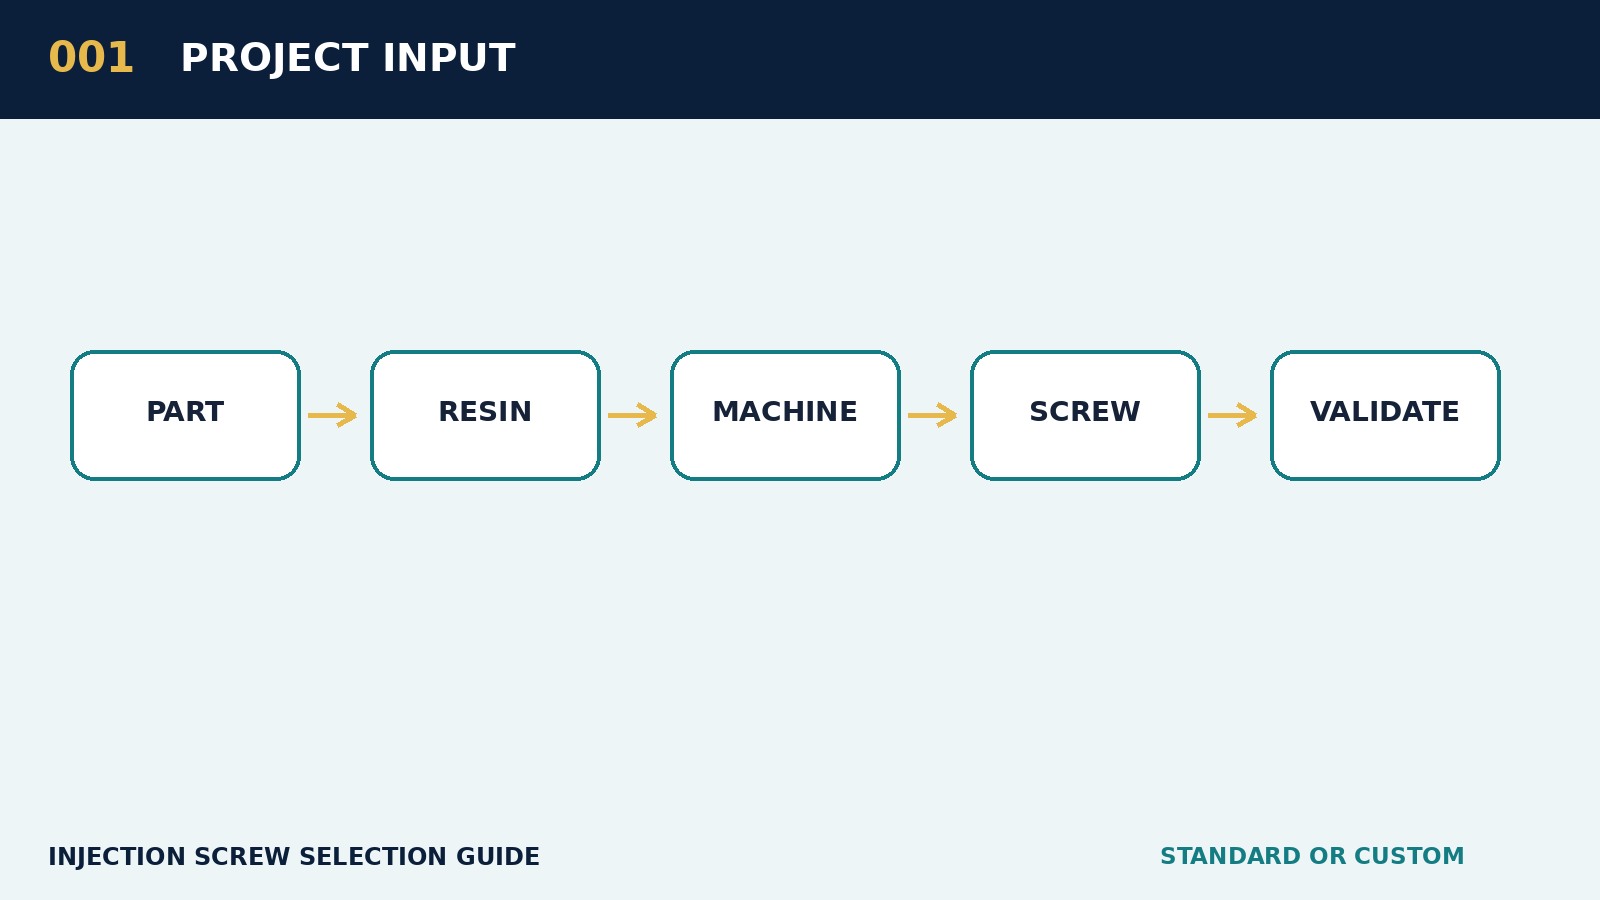
In the new retrofit project, the project manager of the retrofitner does not first have to choose a ready-made model, but rather to identify product sizes, single weights, wall thickness and capacity targets. This step determines whether the subsequent spiral diameter, structure and material grade are well founded.
The core of the demand phase is not to immediately give a screw model, but to convert the client ' s product target into a calculable data. Product weights, project sizes, wall thickness, flow ratio, number of lacquers, flow weights, material plates and target cycles must be placed in the same record; if one of them has not been identified by the customer, it should be clearly marked as a hypothesis and the sales calibre should not be mistaken for final technical condition. It is recommended that customer information be broken down into five groups: products and moulds, raw materials, platforms, process objectives and existing problems. Product end logs of single weight, flowway, number of caves, wall thickness and appearance levels; ratio of feedstock end recorder number, melting finger, filling, flame retardation and retrofitting; terminal logs of tonnage, voltage, screw diameter, maximum travel, injection pressure and plasticization. All data are sourced and are marked, drawn, physical, measured or estimated by clients.
Site information should preferably include both photographs, short videos and data sheets. Photos are used to identify machine interfaces, screw tails and front-end components, video can be observed to measure, buffer and abnormal sound, and data tables are used to calculate the rate of application, the need for plasticization per hour and the length of stay. If only partial information can be obtained, a list should be provided for confirmation, rather than a tentative condition being a definitive conclusion. The focus of the discussion here is on product sizes, single weights, wall thickness and capacity targets, which must correspond to the customer ' s current production conditions and not be limited to the maximum values in machine samples.
In the context of this project, it is proposed to adopt the idea of “building demand tables for products, raw materials, platforms, moulds, and processes”. First, to determine whether the available data support the choice, then to calculate the volume of reductive, pressure and plasticization, and finally to discuss the geometry, front-end components and material handling of the screws. If the standard scheme is able to cover the window, priority should be given to the standard configuration; if the information is incomplete, the risk remains that the screw programme will be disconnected from the actual work situation, then the dedicated structure will be proposed and the increased costs, deadlines and expected benefits will be indicated.
If the above steps are ignored, the most common consequence is that incomplete information leads to a disconnect between the screwdriver programme and the actual work situation. The problems are often manifested in the trial phase of measuring time instability, insufficient stress residuals, buffer drift, unmelted, black spots, colour differentials or increased wear and tear. Continued increase in temperature, back pressure and turn speed at this time may temporarily improve the appearance, but may increase the shearing heat, material degradation and equipment load.
At the time of acceptance, it is recommended that the test period, the time of plasticization, the stability of the mass of the product be the main indicator, and that the temperature of the drums, the turn of the screw, the back pressure, the measurement position, the buffer position, the injection peak pressure and the continuous sample weight be simultaneously recorded. At least three reasonable process points, low, medium and high, are covered to confirm that the programme is not effective under a single parameter. For aluminum manufacturers and vendors, professionalism is reflected in the ability to translate the client language into engineering parameters and to interpret the programme into production, quality, maintenance and cost results that the client can understand. The establishment of a standard process around the new retrofit project would not only improve the accuracy of the selection but also create a reusable machine and application database.