
How fast does a vendor judge when a customer complains about a volatile plasticization?
Release time:2026-09-22
(c) For post-sales engineers, describe the reconciliation method for feedstocks, drying, heating, reversal, wear and tear, and process changes, analyse the determination that screw quality leads to misleading screening and increases the risk of shutdown, and provide recommendations for verification of the use of time lines and exclusion methods to locate the source of change and the timing and repetition failure rate.
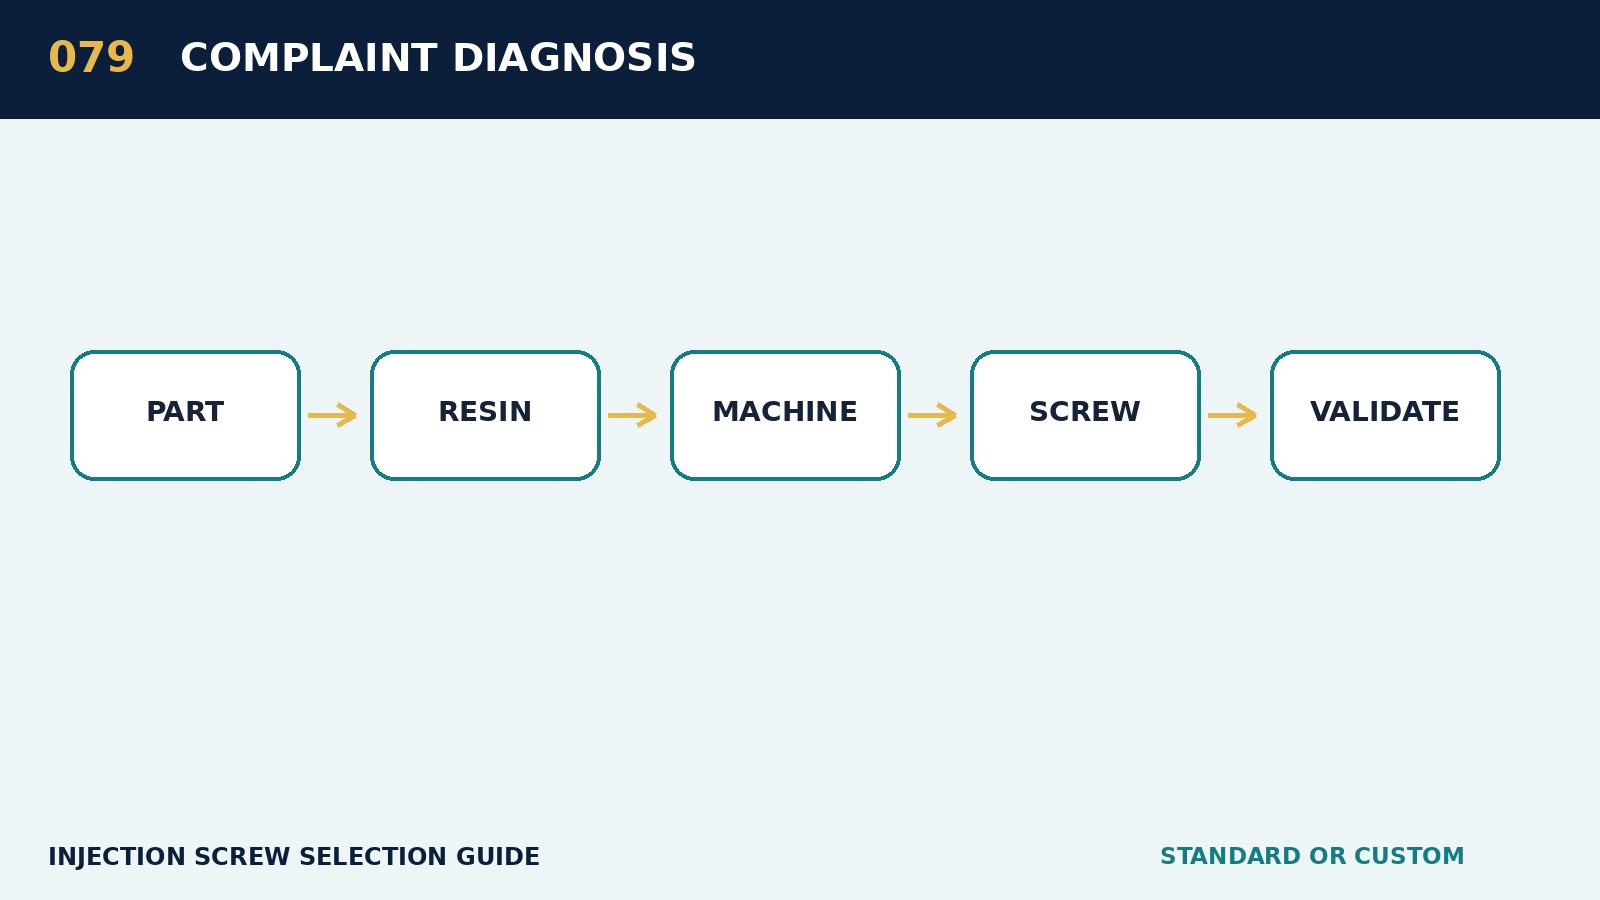
When the project involves the diagnosis of a complaint, the screwdriver programme must start from the real production tasks of the client. After-sale engineers are required to organize raw materials, drying, heating, inversion, wear and tear, and process changes into a set of verifiable, calculable and retroactive entry conditions.
The value of technology sales is to reduce the risk that customers will miss the equipment and accessories. Sales personnel need to close the demand questionnaire, technical evaluation, quotation boundaries, delivery nodes and post-sale recording, so that customers know what data each recommendation is based on, and that internal design and manufacturing teams have consistent information. It is recommended that customer information be broken down into five groups: products and moulds, raw materials, platforms, process objectives and existing problems. Product end logs of single weight, flowway, number of caves, wall thickness and appearance levels; ratio of feedstock end recorder number, melting finger, filling, flame retardation and retrofitting; terminal logs of tonnage, voltage, screw diameter, maximum travel, injection pressure and plasticization. All data are sourced and are marked, drawn, physical, measured or estimated by clients.
Calculates the nominal value to be converted to the actual condition. The machine often uses PS as a reference for the gel weight, which should be revised by density when using other raw materials; the weight of the product should be added to the main course, traffic separation and a reasonable buffer. The larger the diameter of the screw, the greater the theoretical capacity, but the pressure of injections per unit area under the same hydraulic pressure or servo system will decline and the resolution of the measurement of the small amount of the aerosol may also be variable. The focus of the discussion here is on raw materials, drying, heating, inversion, wear and tear, and process changes, which must correspond to the customer ' s current production conditions and not be limited to the maximum values in machine samples.
The implementable option is to locate the source of change using time lines and exclusions. The quoted documents should include both the applicable raw materials, the range of recommended voltage, the permitted turn-off and back pressure, the size of the interface, the material and thermal treatment, and the need for re-evaluation when marking subsequent changes to the material or the mould by the client. This would prevent the use of earmarked programmes in completely different conditions.
The cost of the misconfiguration is not only the screw itself, but also the cut-off, the waste of raw materials, the testing of molds, the delay in delivery and the credibility of customers. Precautionary measures around first determining the quality of the screws would mislead screening and increase the number of stopovers would be more economical than re-routing after problems have arisen; the seller could then move from a mere offerer to a partner capable of carrying technical screening.
Validation focuses on positioning time and repetition failure rates. The test shall use the actual material and representative moulds of the client, retaining the batch number, dry condition, ambient temperature and sample number. When compared to old schemes, equipment, moulds and major process conditions other than screws should be as consistent as possible. Where the information is temporarily incomplete, the pre-selection scope and the list to be confirmed may be provided, but it should not be considered a final commitment. Freezing of configurations after completion of raw materials, drying, heating, reversal, wear and tear and changes in process by the client can reduce erroneous orders and facilitate the production, testing, installation and sale of the same version of data.