
Impact of changes in the root diameter of the screw on the strength of the twister and the volume of the screwdriver
Release time:2026-09-20
The root diameter determines at the same time the capacity of the core of the screw to carry the cross-section and of the snail, which is a direct trade-off between strength and delivery capacity. From the principles of work, selection conditions, common risks and certification methods, the effect of a change in the root diameter of the screw on the strength of the twister and the volume of the screws helps to stabilize the retrofitting plant and to reduce the full life cost of the screw drum.
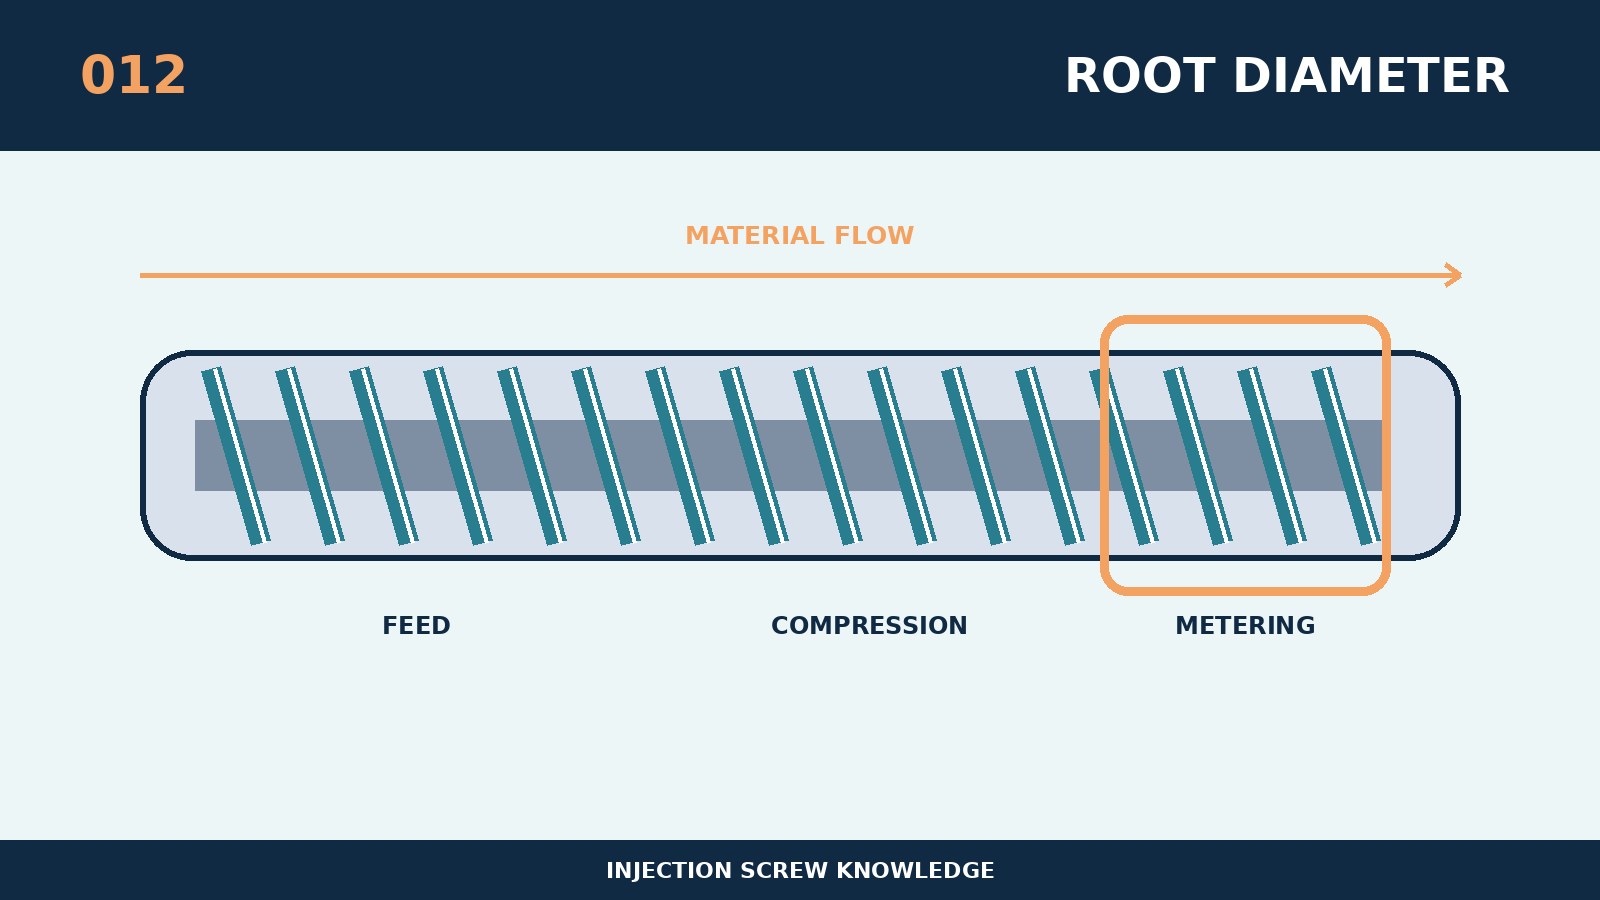
The effect of a change in the root diameter of the screw on the strength of the twist and the volume of the screws is not an isolated parameter, but a key condition for influencing transmission, temperature rise, pressure and repetition in the plasticization system. The core is the root diameter, which simultaneously determines the capacity of the core of the screw to carry the cross-section and of the snail, and is the direct trade-off between strength and delivery capacity. An increase in the root diameter increases the anti-twirl face, but reduces the volume of the snail; a reduction in the root diameter increases the volume but increases the resilience of the reversal. Structural parameters are interconnected and any local modifications are evaluated in the complete path of transport, melting, mixing, metrology and cleaning. The design evaluation is to distinguish between “scales can be installed” and “processes can be stabilized”, the former only resolve mechanical interfaces, and the latter relate to plasticization efficiency and product quality. Nominal specifications are therefore only the starting point, and the final conclusions must serve the actual resin, product and volume rhythm.
When customizing around the "Impact of changes in the root diameter of the screw on the strength of the twist and the volume of the screw," first collects the actual dimensions of the equipment model, the original screw and the material drum, the driving power, the resin number and the filling system, the sum of the single simulator, the cycle and the existing defects. The specific selection principles for this topic are: high viscosity, high filling or large diameter screws should give priority to nuclear peak twists, key connections and root corners. The same mass and the same cooling time should be used for the test to record the amount of plasticization and energy consumption at a low, medium and high three-stage rotation, respectively. The technical agreement should include quantifiable provisions for size benchmarks, key communications, material status and acceptance methods so that new, old and subsequent restorations can be compared under the same criteria.
The most important defence against the failure of the subject is the exhaustion cracks that may occur as a result of small roots or a concentration of round-angle stress, which in turn may lead to insufficient plasticization and high cutting. A curved envelope of the normal package should be created to see if the abnormal cycle occurs at the feed, later-storage, injection start or voltage stage. For on-site processing, only one main variable is changed each time and the measurement time, twist, melting temperature, mat, injection pressure and product weight are aligned to the same pattern. If production is to be sustained by excessive temperature, turn speed or back pressure, the use of parameters to mask structures, wear or collage should be discontinued.
Validation of the "effect of a change in the root diameter of the screw on the strength of the twister and the volume of the screws" can be used as a replicable option: combined with a record of the electric twister, calculation of a limited object or strength, actual plasticization and a combination of periodic no-loss tests. Acceptance and inspection reports should include both actual measurements and location of points, rather than only “qualified”; critical sizes should also be kept with calibration and temperature conditions. Inquiries to suppliers should also be accompanied by information on resins and fillings, risk of flame retardation or corrosion, total weight of products and fluids, photographs of available screws and equipment curves. The programme is considered to have a stable engineering value when the detection data, the good product rate, the timing of the switch and the unit cost of the eligible goods are improved.