
How to avoid a bridge and slide around a screwdriver feed mouth
Release time:2026-09-20
The feed mouth area needs to allow the particles to fall into a spiral and to form a stable solid transport through temperature and friction conditions. The working principles, selection conditions, common risks and validation methods illustrate how the structure around the screwdriver mouth avoids bridge-building and slippage, helps the retrofitting plant to stabilize and reduce the full life cost of the screwdriver.
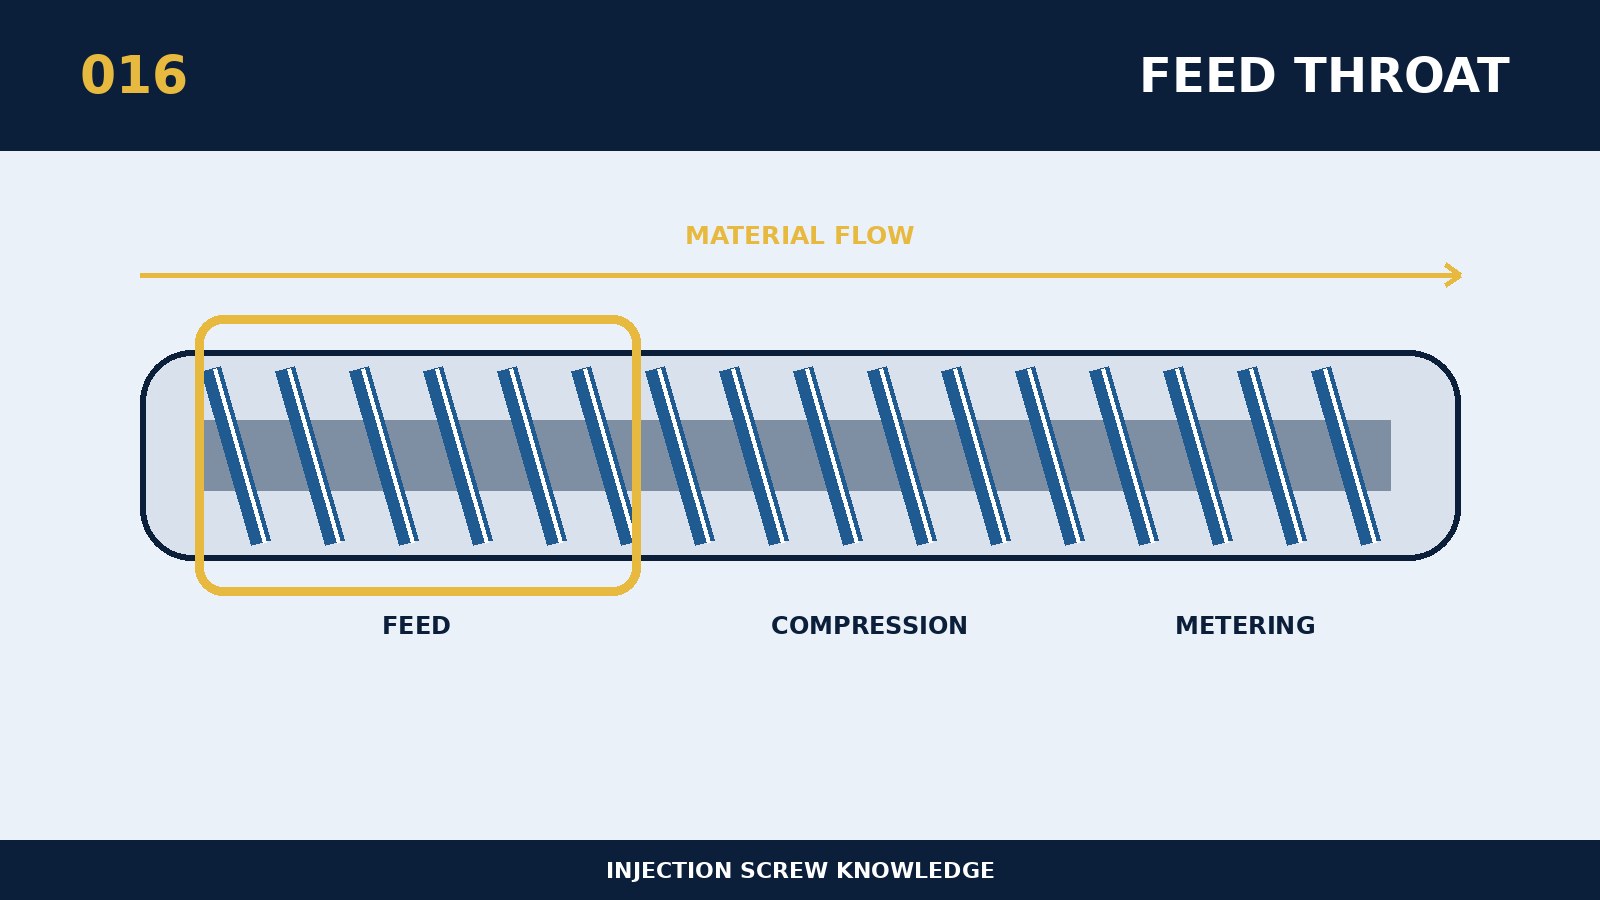
The determination of how the structure in the vicinity of the screwdriver feed mouth avoids bridge and slippage should begin with the placement of structural dimensions, material behaviour and actual production loads in the same logical chain. At its core is the need for feed mouth areas to allow particles to fall smoothly into the coil ' s snails and to create stable solid transport through temperature and friction conditions. The size of the feed mouth, the depth of the first concourse, the angle of the plume, the cooling of the additional section and the state of the particle surface interact. Structural parameters are interconnected and any local modifications are evaluated in the complete path of transport, melting, mixing, metrology and cleaning. The selection programme should draw the boundary of production, temperature rise, twirl and time of stay before determining whether the parameter pushes the work to an uncontrolled area. Nominal specifications are therefore only the starting point, and the final conclusions must serve the actual resin, product and volume rhythm.
When customizing around "how to avoid bridges and slips" in the vicinity of a screwdriver mouth, first collects the size of the equipment model, the original screw and the material drum, the driving power, the resin plate number and the filling system, the single mass, the cycle and existing defects. The specific selection principles for this topic are that the flow of the material and the volume of the first circle should be specifically assessed in the form of retrospect, soft material, powder or lubricant formulation. The operational evaluation should not only look at single-modules, but at least cross three stages of complete warming, steady-state production and a moratorium on restarting. The technical agreement should include quantifiable provisions for size benchmarks, key communications, material status and acceptance methods so that new, old and subsequent restorations can be compared under the same criteria.
The most important defence against the failure of the subject is that overheating of the material makes the particles softened and glued early, and overcooled condensers bring water and cause silver silk. Bad pictures are bound to the same pattern as the equipment curve and raw material records, otherwise only the defective name cannot be judged to have been caused by a screw. For on-site processing, only one main variable is changed each time and the measurement time, twist, melting temperature, mat, injection pressure and product weight are aligned to the same pattern. If production is to be sustained by excessive temperature, turn speed or back pressure, the use of parameters to mask structures, wear or collage should be discontinued.
This replicable approach can be used to verify how the structure around the screwdriver mouth avoids bridge and slide: observation of the continuity of the cavity, the temperature of the cavity, the sign of an empty rotor of the screw and the measurement changes under the different material positions. The point of review of continuous production should be triggered by production or tonnage of raw materials, which would better reflect the true load of the screw than a mere calendar time. Inquiries to suppliers should also be accompanied by information on resins and fillings, risk of flame retardation or corrosion, total weight of products and fluids, photographs of available screws and equipment curves. The programme is considered to have a stable engineering value when the detection data, the good product rate, the timing of the switch and the unit cost of the eligible goods are improved.