
POM Polysalphate Particle Characteristics and Safety Motion Recommendations
Release time:2026-09-20
Crystal constriction for POM Thermal stabilization of boundaries and low friction applications that indicate temperature security for pressure and refuelling. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
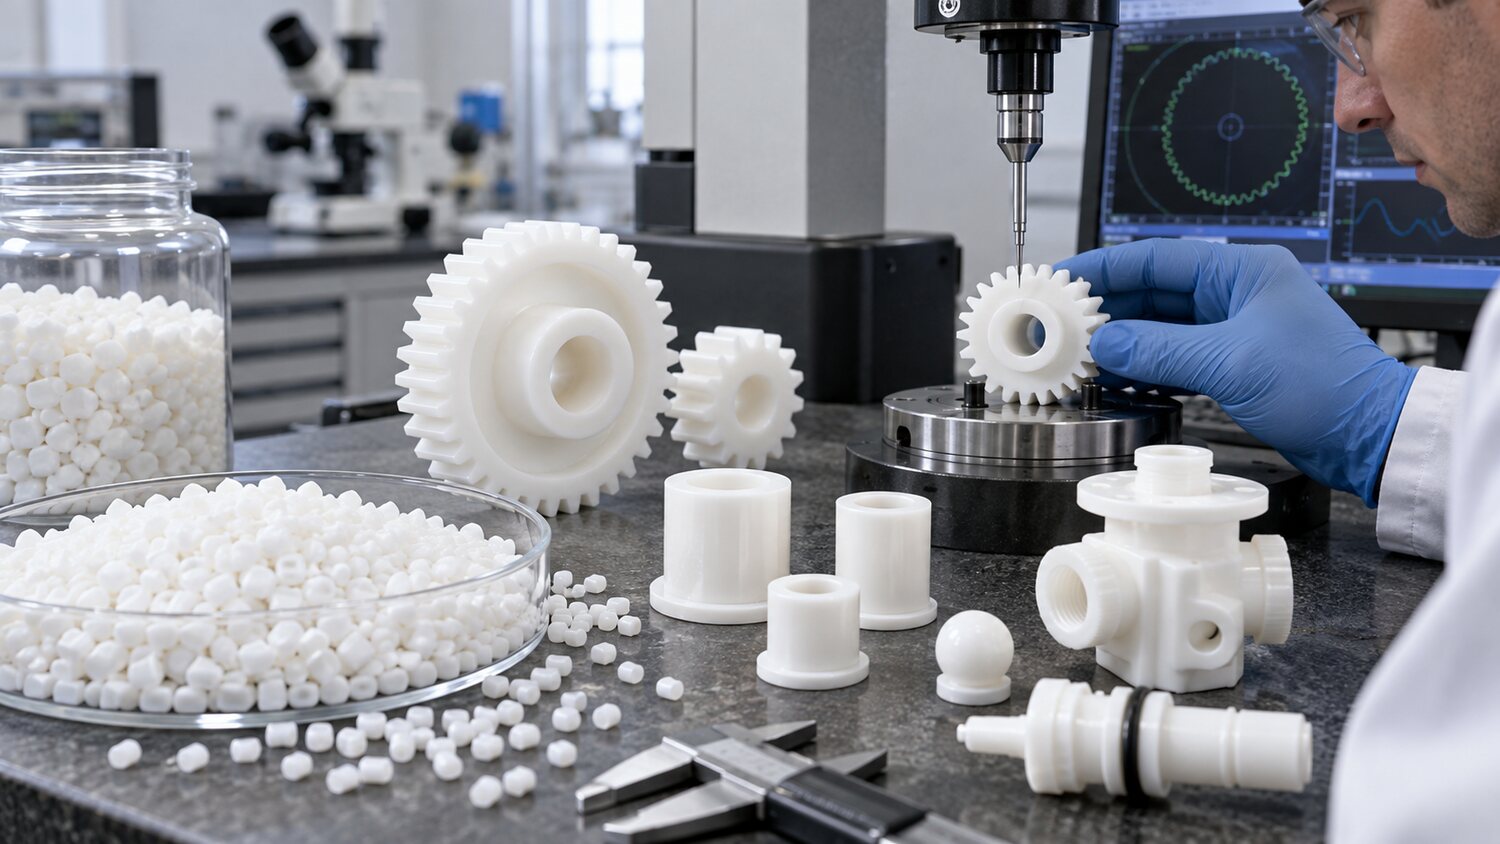
POM has rigidity, low friction, fatigue and size stability, often used in gears, slides, valves, zipping and precision mechanical parts. It is a semi-crystal material, which is more sensitive to temperature, pressure and modulus by flow and formation contraction. POM is divided into different systems such as homogeneity and congregation, and the processing window and thermal stability are not identical, and a specific number must first be identified. Although some POM requirements for drying are not as stringent as those for PC and PA, damp, packaging damage, mother colour or respirator contamination may still affect surface and performance, and pre-drying should be performed on the basis of supplier information.
The most important thing for POM is to avoid overheating and excessive stay. The temperature of the drum shall be kept within the permitted range of the plate, and the screw speed and back pressure shall not be too high, and it shall be subject to the prescribed charge or cooling when waiting. In the event of irritating scents, smoke, darkening colours or an abnormal melting bubble, the continued heating and geling should be stopped immediately, ventilated in accordance with site safety procedures, cleaned up and the cause identified. POM shall not mix directly with PVC or other chlorine-containing materials, which may be hazardously decompositioned at high temperatures; the refuelling and clean-up of the aircraft shall be based on empirically compatible materials and steps.
Because POM crystals are condensed more clearly, sophisticated gears and valves require stable temperature, reasonable pressure and even cooling. The water pressure controls the reduction of water and internal stress. Too little water is too early to freeze, making it impossible to refill the thick wall at the far end; excessive pressure can also lead to difficulties, large sizes or residual stress. Arrays should be judged by combination of watering, wall thickness, cooling and molecular orientation. For gears, except for diameters and apertures, changes in the dimensions of the circle, gear, rodent noise and after placement are also checked.
POM has a better mobility, and the screw design should focus on smooth transport, even plasticization and the reduction of the arctic angle, without the need for a very high compression ratio to a reinforced cut. Unresolved reverse ring seals can cause volatilisation, directly affecting the weight and size of the precision. Long-term black dots or yellow transformations often come from the nozzles, anti-reversible components and snail-head demurrage areas, which should be addressed through equipment overhauls rather than continuing to increase temperature cleaning. Recoverants are used with strict control over source, heat history and ratio and are verified through friction, fatigue or size tests. Secure borders, stop times and refuelling procedures should be as important as product parameters.