
Why do PVC screws usually use a mild compression design?
Release time:2026-09-20
The PVC thermal stabilization window is narrower, plasticization relies on controlled shearing and external heating, and local overheating can cause decomposition. From the principles of work, selection conditions, common risks and certification methods, it is possible to explain why the PVC screw is usually designed with a mild compression to help the retrofitting plant stabilize plasticization and reduce the full life cost of the cylinder.
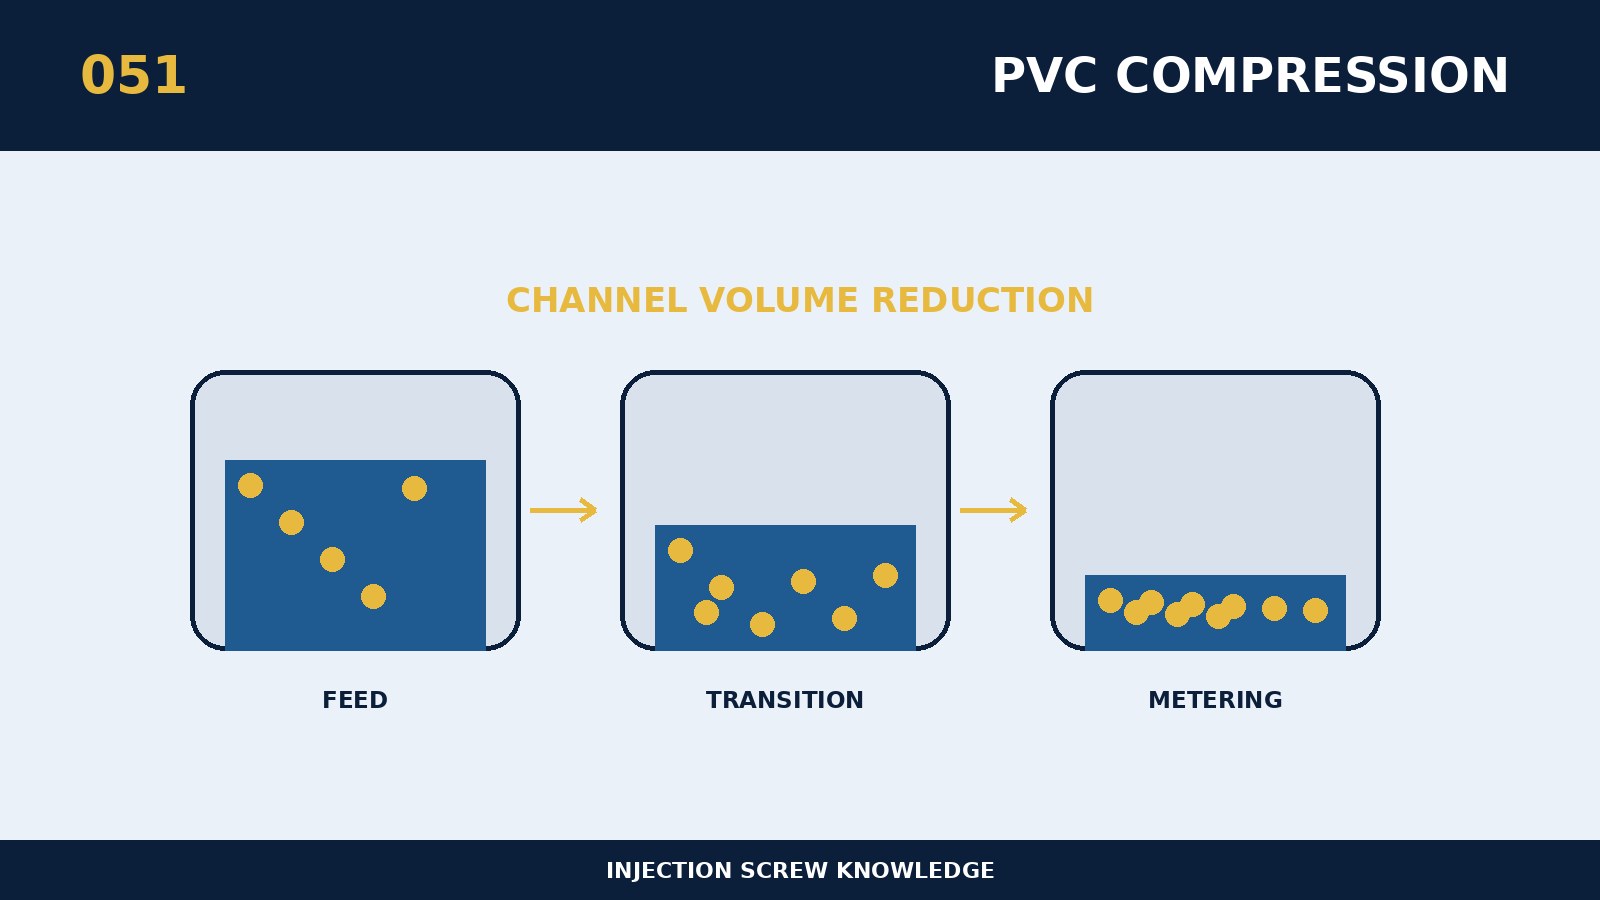
The determination of why the PVC screw is usually designed with a mild compression, starting with the placement of structural dimensions, material behaviour and actual production loads in the same logical chain. At its core, the PVC thermal stabilization window is narrower, plasticization relies on controlled shearing and external heating, and local overheating can cause decomposition. Temperature compression and smooth transitions can reduce high-pressure shearing points while helping to stabilize transmission and exhaust. Compression ratios must be understood in conjunction with the length of the compressed segment, the conductor, the depth of the tank, the back pressure and the material flow, and the individual comparison is easily miscalculated. The selection programme should draw the boundary of production, temperature rise, twirl and time of stay before determining whether the parameter pushes the work to an uncontrolled area. Nominal specifications are therefore only the starting point, and the final conclusions must serve the actual resin, product and volume rhythm.
When customizing around "Why the PVC screws usually use a mild compression design", first collects the size of the equipment model, the original screw and the material drum, the driving power, the resin number and the filling system, the sum of the single simulator, the cycle and the existing defects. Specific selection principles for the topic are: plasticizers, stabilizers, fillings, hard soft type and production target design in the formulation. The high-yield project should also reconcile the heat load of the speed-reducing box with the electric power to avoid a long-term overload of the propeller itself. The technical agreement should include quantifiable provisions for size benchmarks, key communications, material status and acceptance methods so that new, old and subsequent restorations can be compared under the same criteria.
The most needed failures of the subject are: dead angles, sharp edges, hypercompression and stopovers that produce colour variations, acid gases, corrosion and carbon accumulation. The removed parts shall retain directional markings and record grinding marks, corrosive pits, discoloration and residues in the order in which the loading end reaches the front end, and establish a retroactivity map. For on-site processing, only one main variable is changed each time and the measurement time, twist, melting temperature, mat, injection pressure and product weight are aligned to the same pattern. If production is to be sustained by excessive temperature, turn speed or back pressure, the use of parameters to mask structures, wear or collage should be discontinued.
Validation of the “PVC screw” is usually based on a mild compression design, which can be used as a replicable option: a rectangular, actual temperature, colour, smell, cut-off and metal surface corrosion. If the programme involves new materials or layers, it can be scaled up in stages under controlled production, and the quality of wear and tear is reviewed at each stage. Inquiries to suppliers should also be accompanied by information on resins and fillings, risk of flame retardation or corrosion, total weight of products and fluids, photographs of available screws and equipment curves. The programme is considered to have a stable engineering value when the detection data, the good product rate, the timing of the switch and the unit cost of the eligible goods are improved.