
What's the choice of a high-mixed plastic screw? Colour mother dispersion and colour differential control
Release time:2025-08-07
How does a high-mixed plastic screw choose a colored mother to be separated and colored? First, the plastic plate number and filling ratio are identified, then the plastics specifications, product sizes and mass defects are checked, and the long-range ratio, compression ratio, mixing structures and screw material is finalized. This paper combines information on star-friend screw stations to organize selection, process and validation elements.
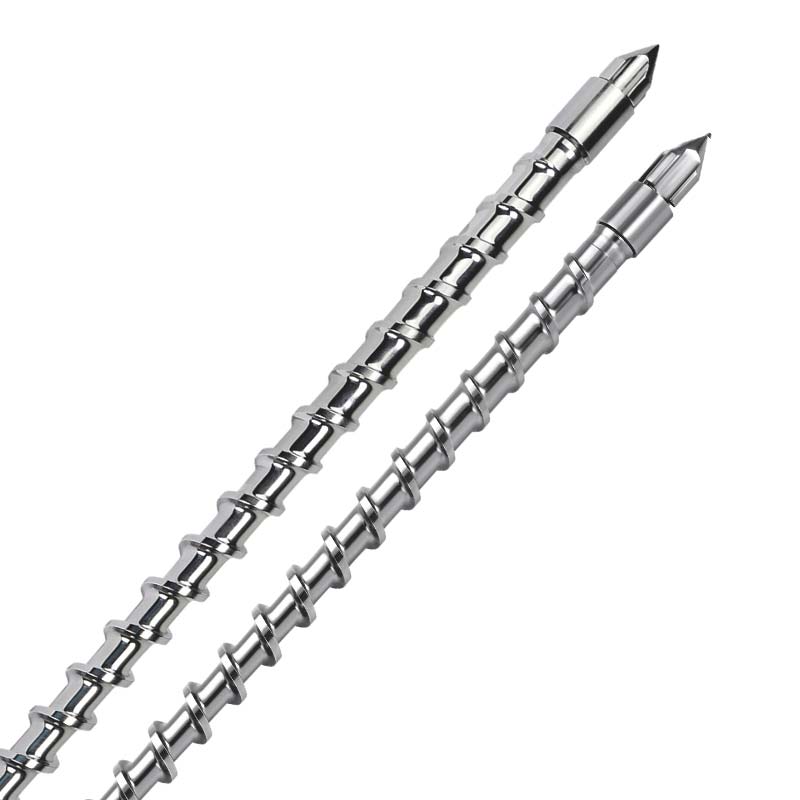
The core conclusion of a high-mixed plastic screw.
First, the plastic plate number and filling ratio are identified, then the plastics specifications, product sizes and mass defects are checked, and the long-range ratio, compression ratio, mixing structures and screw material is finalized.
Key to the formation of a hybrid of chromosomal particles: a solution for a high-mixing capability generically retroplied screw
In the area of mixed mother-particle products, products such as two-colour toys and multi-colour shelles have important market shares based on their rich colour performance. This type of product is usually shaped by a combination of materials such as ABS, PP and PS, and the requirements for colour homogeneity are extremely strict - industry standards require that the same product be within 1.5 colour difference E and not subject to visible chromosomal, florist, etc. However, during the production of common equipment, product waste rates due to the unevenness of the mix tend to be as high as 12-18 per cent, with the incidence of double-coloured toy belt problems exceeding 20 per cent, seriously affecting production efficiency and product quality. This paper will analyse the technical difficulties of the mixing of chromosomal particles, taking into account specific data, and will elaborate on how the high-mixing capability generic plywood screws can be tailored to address the pains of production.
Core mass pain points and technology needs for co-production of coloured mother particles
The essence of chromosomal granule mixing is to spread the chromosomal particles evenly into the matrix melting. Its quality deficiencies stem mainly from fragmentation and uneven mixing. From a micro-level perspective, among the eligible mixed products, the particles are dispersed to a particle size of 5 m, with a deviation of not more than 10 per cent per square millimetre; they exceed 20 m, creating visible chromatoma in the eye; and they are produced mostly by fluctuations in the concentration of the particles in the molten form of more than 5 per cent, resulting in local colour deviations.
Material properties add to the difficulty of mixing: ABS can have a density difference of 0.05-0.1 g/cm 3, which can easily be stratified by weight differences; PP surfaces can be lower, colour particles can be humid, dispersing resistance is 30 per cent higher than ABS; PS molten viscos are more sensitive to shear rates, and when cut short, the mother can easily join into particles with a particle size of 50-100 mm. Normal plume screws, because of their simple mix structure (mostly single threads), have only a 60-70 per cent dispersion of the colored mother, far from meeting the requirement of high evenness.
Technical parameters and performance advantages of a high-mix capability generic piping spiral
Three structural breakthroughs were achieved in the design of the high-mixing capability generic plywood screws to meet the core needs of a mixture of mother particles. The design of strong mixed areas is its core advantage. Sets a double-sniffed coil and a barrier-type cut in the middle of the plume, which is controlled at 0.5-0.8 mm and reduces by more than 50 per cent the normal plume (1.2-1.5 mm), resulting in a strong trajectory mixing at passage. The measured data indicate that the structure has increased the dispersion of ABS-coloured mothers to 95 per cent, and that the average particle size of the mother-colour particles has been reduced from 35 μm to 4.2 μm of the normal plywood screw, fully meeting the requirements of microequilibrity.
In the design of the high-hear-cut plastic scalding skeletal unit, a cosmopolitan structure (the snail length gradually changes from 60 mm to 40 mm) is used, which is accompanied by a deeper snail (15 per cent deeper than the normal snail) and stabilizes the shear rate at 200-300s-1 and 2-3 times that of the normal snail (80-120s-1). This high shearing can effectively break the colored parent. – Tests on the PP material show that the rate of a colored parent reunification fell from 28 per cent to 3.5 per cent of the general platinum screws and the rate of flower-type defects from 18 per cent to 1.2 per cent. At the same time, the temperature-control accuracy of the cut part was raised to ±1 °C, avoiding chromosomal decomposition due to local overheating (230 °C for the ABS colored mother) and the actual working temperature of the plume bolts was stabilized at 210 ± 0.5 °C.
In view of the frequent replacement of materials by production characteristics and the use of a fast-dismantling structure, the co-ordinated gap between the retrofits and the drums is controlled at 0.1-0.15 mm (0.2-0.3 mm for the general retrospect), which ensures both plastic efficiency and rapid disassembly cleaning. The test showed that the cleaning time for the replacement of the colored mother had been reduced from 45 minutes to 12 minutes for the normal plating screw, and that the amount of residual cleaning had been reduced by 80 per cent, significantly reducing the waste of material during the changeover.
Validation of effects in practical application
Data on the production of a toy company show that, following the introduction of a high-mix capacity generic plating screw, the success rate for two-colour toys increased from 82 per cent to 99.3 per cent. In particular, the waste rate due to the unevenness of the mix fell from 15 per cent to 0.7 per cent, the color belt deficiency rate from 20 per cent to 0.5 per cent, and the colour difference E was stabilized at 0.8-1.2, fully meeting the industry ' s high-end standards. Tests on PS multi-colour crust showed a 40 per cent increase in the dispersive homogeneity of the mother and a decrease in the deviation in the distribution of the mother particles per square millimetre from 18 per cent to 6 per cent.
In terms of production efficiency, as a result of reduced back-to-work and clean-up time, the efficient operation of equipment increased from 75 per cent to 92 per cent, and daily production increased by 28 per cent. In terms of material utilization, the waste of re-colored transitional material was reduced from 5 kg per batch to 0.8 kg per batch. On the basis of eight batches per day, annual savings on raw materials cost approximately $520,000.
The high-mixing capability generic piping screws have fundamentally addressed the three pain points of the mixing of the chromosomal particles through the design of strong-mixed structures, high-cut cutting and easy-cleaning. This professional solution will become the core option for multi-colour retrofitting enterprises as the demand for product colour diversity and homogeneity increases in the consumer market, and will drive the industry from “qualified production” to “precision manufacturing”.
Data to be recorded before implementation
- Material integrity number, filling ratio, flame-retarding system, refill ratio and dry condition.
- Note plastics brand, model, screw diameter, voltage, back pressure, turn speed and current screw structure.
- Indicators of product size, wall thickness, appearance or strength, and current adverse phenomena and frequency of occurrence.
- Continuous production cycle, refuelling frequency, machine clean-up method, wear and tear record and planned useful life.
How to validate the adjustment results
It is recommended that the current process baseline be established, followed by a single-variant test model. Each round records the measurement of time, melting temperature, product weight, formation cycle and bad rate, avoiding multiple parameters being changed at the same time to determine the cause. The parameters in the text are used to illustrate design thinking and should not replace material supplier data and on-site safety protocols.
What kind of support is a star-friend screw?
The Starfleet Mechanical Equipment Co. Ltd. (Starfeng) provides a reset of material and work evaluation, screw structure, base and surface treatment options, non-spectrum customization and trial modelling issues around high-mixed plume. The submission of information on raw materials, equipment and products could lead to more targeted programmes.
Ask for customized screws immediately, or check firstNote plastic screw productwithNote Plastic SolutionsI don't know.