
How's the two-stage compression of the exhaust screw working?
Release time:2026-09-20
The exhaust screws first complete the initial melting and pressure reduction, then release water vapour and volatilizers at the vent and then recompress measures. The working methods, selection conditions, common risks and validation methods show how the two-stage compression structure of the exhaust screw works, helping the retrofitting plant to stabilize plasticization and reduce the full life cost of the screw drum.
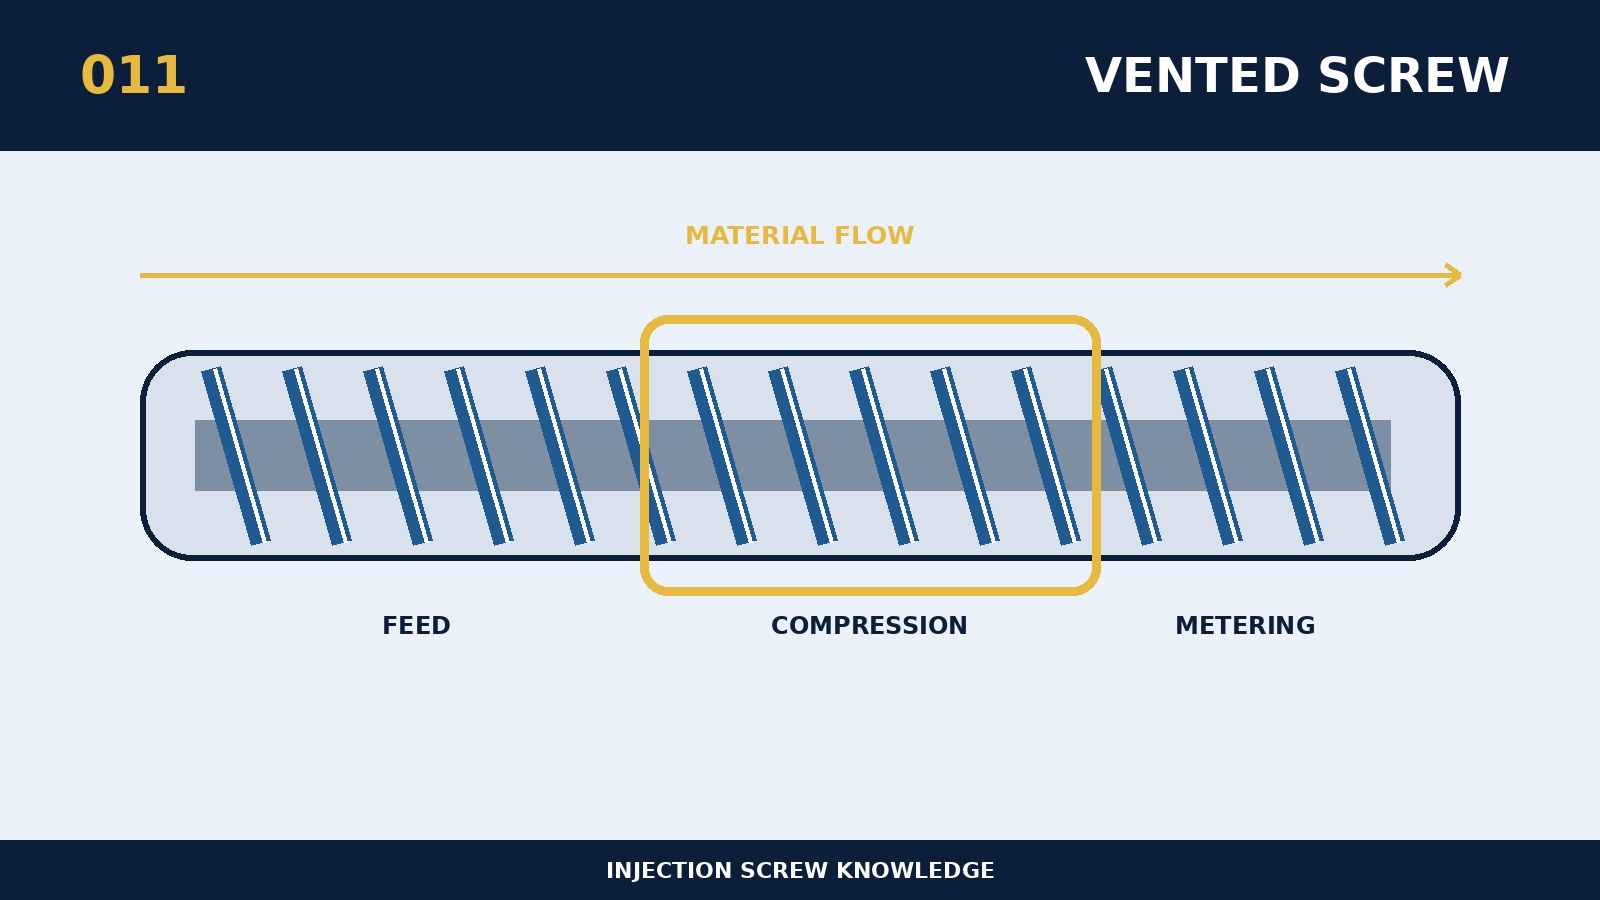
To determine how the two-stage compression structure of the exhaust screw works, the first is to place the size of the structure, material behaviour and actual production load in the same logical chain. At its core, the exhausting screws complete initial melting and pressure reduction, release water vapours and volatilizers at vents and then recompress measures. The first measurement segment must be balanced with the second transport segment relay, and the vent area is overfilled and under-capacity. Structural parameters are interconnected and any local modifications are evaluated in the complete path of transport, melting, mixing, metrology and cleaning. The retrofitting of old machines could begin with the re-establishment of the existing superstitious model, which compares the volume, intensity and heat history of old and new programmes with the same benchmark. Nominal specifications are therefore only the starting point, and the final conclusions must serve the actual resin, product and volume rhythm.
When customizing around “how to work on a two-tiered compression structure of an exhaust screw”, the equipment model, the original screw and the material drum are first collected for measuring size, driving capacity, resin number and filling system, single mass, cycle and existing defects. Specific selection principles for this topic are: water-containing, volatilizing or recycling applications that assess exhaust structures, together with stable vacuums and reasonable temperature setting. The high-yield project should also reconcile the heat load of the speed-reducing box with the electric power to avoid a long-term overload of the propeller itself. The technical agreement should include quantifiable provisions for size benchmarks, key communications, material status and acceptance methods so that new, old and subsequent restorations can be compared under the same criteria.
The most intrepid failure of the subject is that vent volume, insufficient vacuum or two-stage transport imbalance can cause gaseous, silver silk, measuring fluctuations and material outbursts. If abnormalities occur only in one of the resins, they should focus on their viscosity, filling, corrosiveness and recommended temperature and should not be directly classified as mechanical failure. For on-site processing, only one main variable is changed each time and the measurement time, twist, melting temperature, mat, injection pressure and product weight are aligned to the same pattern. If production is to be sustained by excessive temperature, turn speed or back pressure, the use of parameters to mask structures, wear or collage should be discontinued.
This replicable option could be used to verify “how the two-stage compression structure of the exhaust screw works”: monitoring the vent vacuum, volatilizers, measuring time, product gaskets and impurities under different back pressure. The results of the validation should be the denominator of the eligible products, while counting the time spent on energy consumption, cleaning, stoppage and maintenance, which is closer to real value than a separate comparison of the purchase price. Inquiries to suppliers should also be accompanied by information on resins and fillings, risk of flame retardation or corrosion, total weight of products and fluids, photographs of available screws and equipment curves. The programme is considered to have a stable engineering value when the detection data, the good product rate, the timing of the switch and the unit cost of the eligible goods are improved.