
How the fresco width and cleavages affect leakage flows and wear
Release time:2026-09-20
Plumb width affects carrying area, friction heat and leak pathways, and side-processing quality also affects material retention. The working principles, selection conditions, common risks and certification methods illustrate how plume width and cleavage affect leakage flows and wear and tear, helping to stabilize the retrofitting plant and reduce the full-life cost of the screw drum.
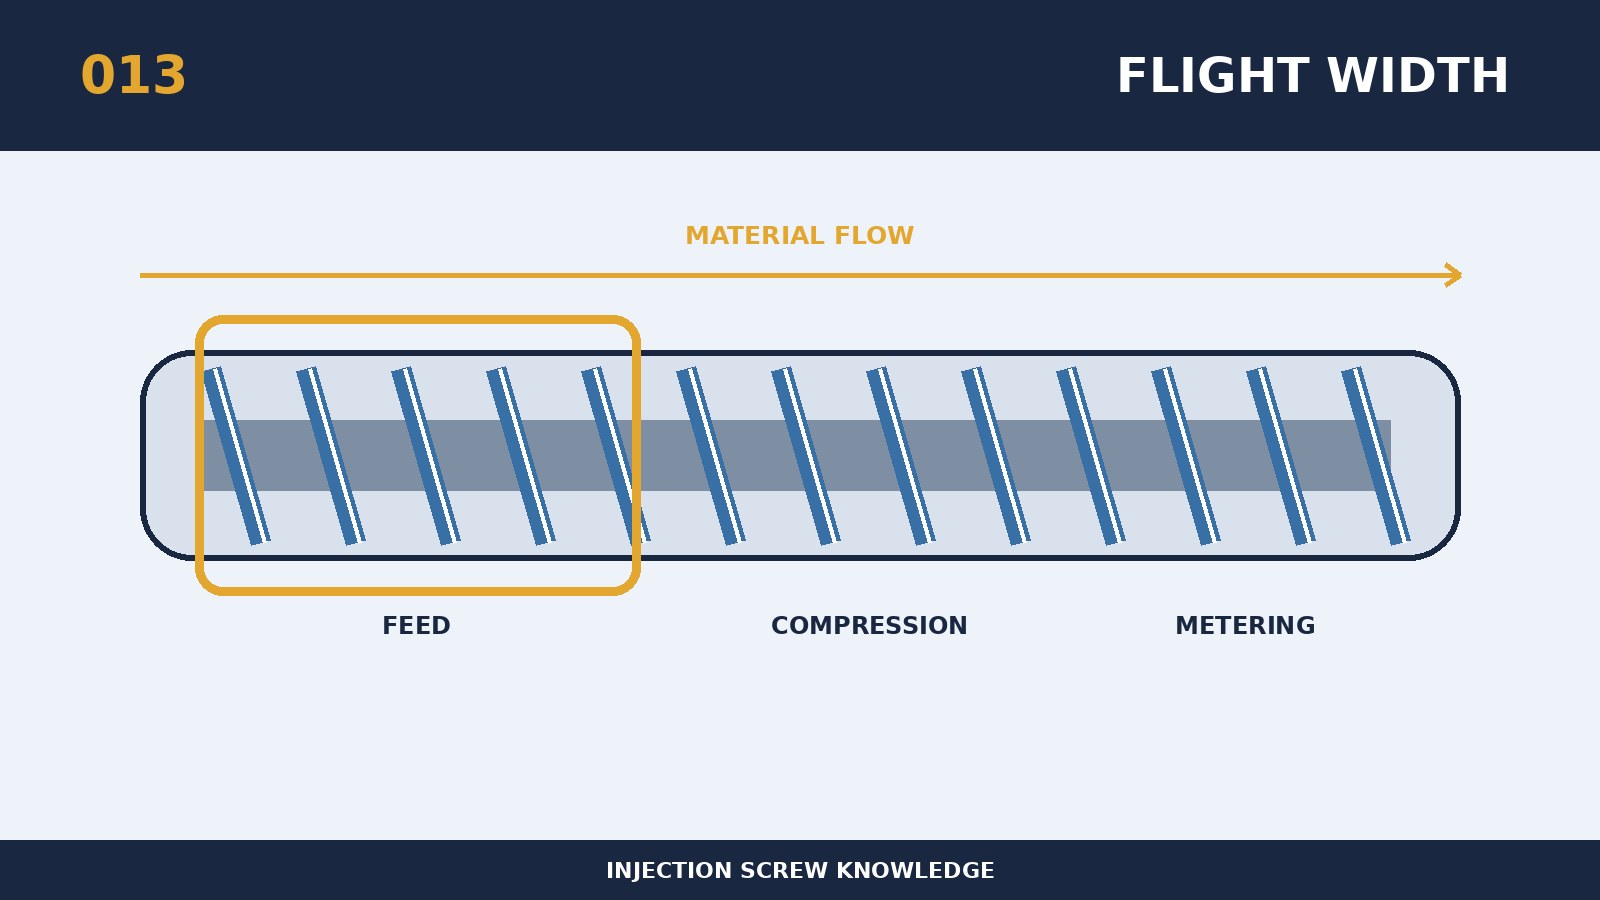
In the screw selection or failure analysis, how the plume width and the cleavage affect the leakage stream and wear and tear is often simplified as a specification, but in fact needs to be explained in conjunction with the full performance. At its core is the plume width which affects the carrying area, friction fever and leak pathways, and the quality of side processing is also related to material retention. Broader fliers favour carrying but increased areas of friction, while narrower fliers are more sensitive to wear and oscillation. Structural parameters are interconnected and any local modifications are evaluated in the complete path of transport, melting, mixing, metrology and cleaning. If the same platform is to cover a variety of resins, the three extremes that are the most difficult to melt, the most afraid of cutting and the most susceptible to degradation are applied separately. Nominal specifications are therefore only the starting point, and the final conclusions must serve the actual resin, product and volume rhythm.
When customizing around “how the pyrotechnic width and cleavage affects leakage flow and wear”, first collects the size of the equipment model, the original screw and the material drum, the driving capacity, the resin plate number and the filling system, the single mass, the cycle and existing defects. The specific selection principle for this topic is that the width should be determined in combination with the diameter of the screw, the silos of the material, the surface hardness, material corrosiveness and the processing axle. The refuelling or recoloring process is subject to a separate assessment, as residuals, clean weights and opening black spots can expose dead corners that are not readily visible in steady-state production. The technical agreement should include quantifiable provisions for size benchmarks, key communications, material status and acceptance methods so that new, old and subsequent restorations can be compared under the same criteria.
The most needed to prevent the failure of the subject was the increase in the return flow of the melting, the decrease in plasticization and the difficulty of removing the black spots, following the expansion of the side-lapse, crumbling or gap. Short-term increases in temperature or back pressure cover part of the structural problem but cannot be a long-term response if the twist, degradation or cycle deteriorates simultaneously. For on-site processing, only one main variable is changed each time and the measurement time, twist, melting temperature, mat, injection pressure and product weight are aligned to the same pattern. If production is to be sustained by excessive temperature, turn speed or back pressure, the use of parameters to mask structures, wear or collage should be discontinued.
This replicable approach can be used to verify how “plugging width and cleavage affect leakage flow and wear”: measurements of the plume width, outer diameter, inner diameter of the drum and local wear and tear bands, as compared to new sizes and energy trends. The screws, drums and reversible rings are proposed as side acceptances, since single-sizes do not represent a suitable axis of the combination gap with the heat. Inquiries to suppliers should also be accompanied by information on resins and fillings, risk of flame retardation or corrosion, total weight of products and fluids, photographs of available screws and equipment curves. The programme is considered to have a stable engineering value when the detection data, the good product rate, the timing of the switch and the unit cost of the eligible goods are improved.