
How does a screw compression work compared to changing the cooler temperature?
Release time:2026-09-20
Changing the compression ratio will change the ratio of mechanical heat, so the temperature of the old screws cannot be replicated mechanically. From the working principles, selection conditions, common risks and validation methods, how the screw compression ratio changes the cooler temperature, helps the retrofitting plant to stabilize plasticization and lower the full life cost of the screw drum.
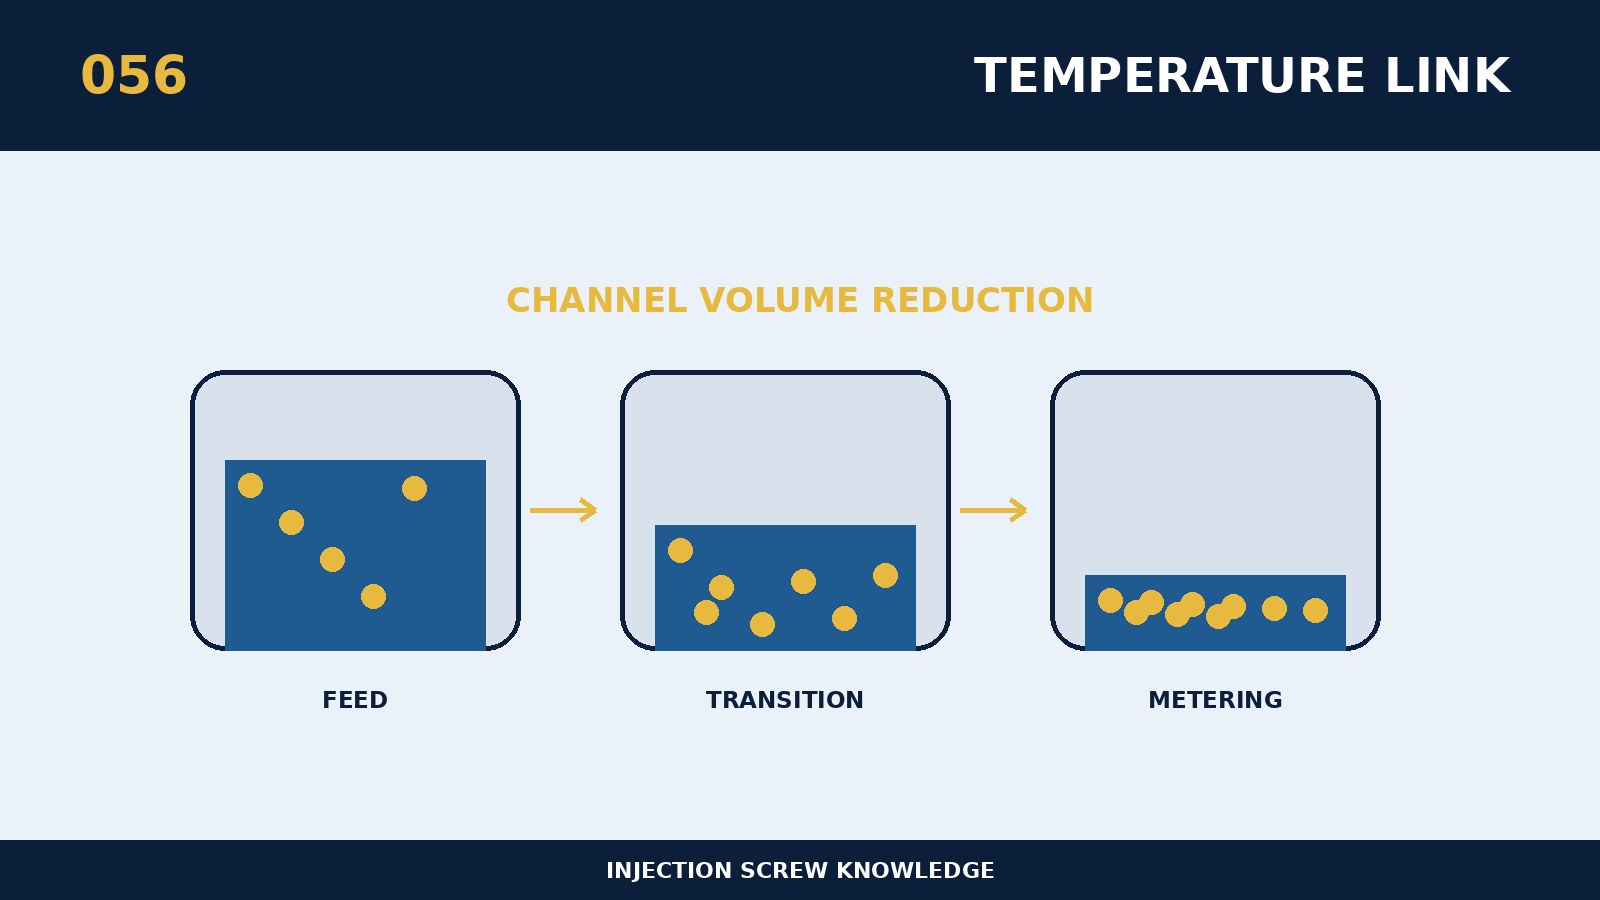
A determination of how a spiral compression is associated with a change in the cooler temperature begins by placing structural dimensions, material behaviour and the actual production load in the same logical chain. The core is that changing the compression ratio changes the ratio of mechanical heat, so that the temperature of the old screws cannot be replicated mechanically. Repression enhancements may require a reduction in some of the temperature zone settings, while moderate structures may be more dependent on external heat transfer. Compression ratios must be understood in conjunction with the length of the compressed segment, the conductor, the depth of the tank, the back pressure and the material flow, and the individual comparison is easily miscalculated. Parameter decision-making can be based on a failure push: short-shot, black spot, product fluctuations and overloading are listed first, and then the geometrics are identified to block the failure chain. Nominal specifications are therefore only the starting point, and the final conclusions must serve the actual resin, product and volume rhythm.
When customizing around the "snack compression ratio changes the temperature of the rear drums" the equipment model, the original screw and the material drums are first collected, the size of the measurements, the driving capacity, the resin number and the filling system, the sum of the single simulator, the cycle and the existing defects. The specific selection principle for this topic is that the actual melting temperature rather than the screen set value should be an important basis for a linkage adjustment. The operational evaluation should not only look at single-modules, but at least cross three stages of complete warming, steady-state production and a moratorium on restarting. The technical agreement should include quantifiable provisions for size benchmarks, key communications, material status and acceptance methods so that new, old and subsequent restorations can be compared under the same criteria.
The most important defence against the failure of the subject is that, if the structure is modified at the same time and the temperature is significantly increased, it will be impossible to distinguish between sources of defects and may mask melting. If abnormalities occur only in one of the resins, they should focus on their viscosity, filling, corrosiveness and recommended temperature and should not be directly classified as mechanical failure. For on-site processing, only one main variable is changed each time and the measurement time, twist, melting temperature, mat, injection pressure and product weight are aligned to the same pattern. If production is to be sustained by excessive temperature, turn speed or back pressure, the use of parameters to mask structures, wear or collage should be discontinued.
This replicable approach can be used to verify “how screw compression is associated with changing the cooling temperature of the rear drums”: a phased, fixed turn-rate back pressure, and fine-tune after measuring actual melting temperature, measuring time, twisting and product performance. Acceptance and inspection reports should include both actual measurements and location of points, rather than only “qualified”; critical sizes should also be kept with calibration and temperature conditions. Inquiries to suppliers should also be accompanied by information on resins and fillings, risk of flame retardation or corrosion, total weight of products and fluids, photographs of available screws and equipment curves. The programme is considered to have a stable engineering value when the detection data, the good product rate, the timing of the switch and the unit cost of the eligible goods are improved.