
Linking diagnostic methods for short-shot flight to shrink mercury.
Release time:2026-09-20
The priority adjustment is judged from the point of view of the mechanism of the defect, so that the multiple parameters are not changed at the same time and the problem shifts. This paper gives recommendations for actionable abbreviators in terms of material properties, temperature, speed, pressure, cooling and common defects.
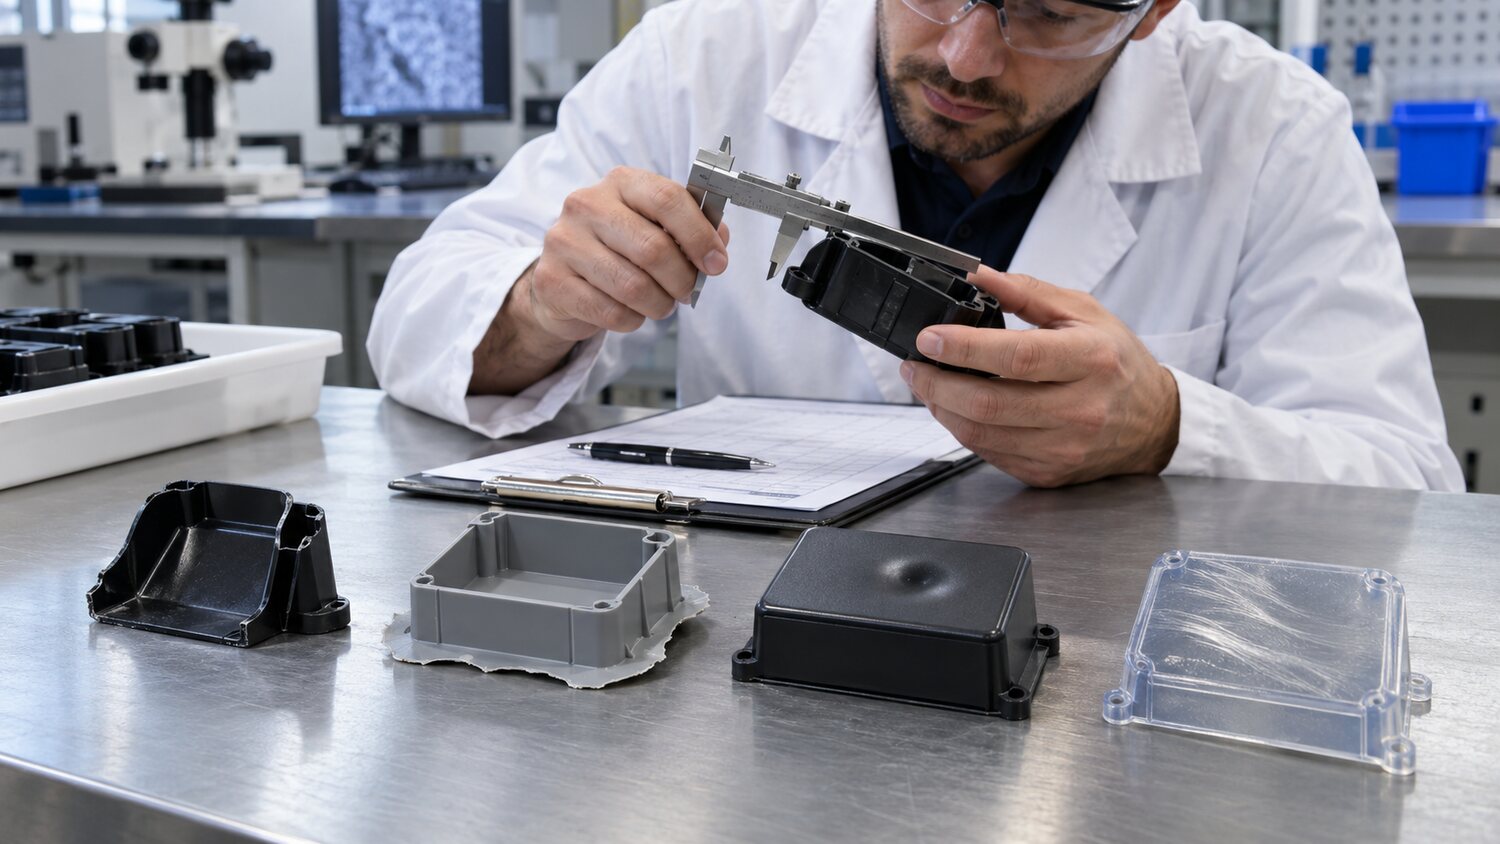
Short-shot, fly-side, water shrunk and silver silk appear to be four separate defects, often caused by the same set of underlying conditions. Short-shots may come from insufficient voltage, actual velocity constraints, low temperature of material or molluscs, poor venting, the reversal of loop flow and too small watering; flying edges may come from late switching, high pressure, inadequate locking power, spectrogenic damage to the molds, or low smelting. The transfer is preceded by a confirmation of the location, frequency of occurrence and mass of the product, and the examination of the pressure curve and the material cushion. If the weight of each model changes, priority should be given to the measurement and reversal issues rather than to fine-tuning the external parameters.
Water shrinks usually occur in areas where thick walls, spasms, poles or mouths are inadequate. It should first verify whether the watering is too early to be closed, then adjust the pressure pressure and the time of effective pressure preservation, and check for local cooling. If water shrinks as a result of increased pressure, but there is a flight edge or internal stress, it is suggested that the application of the mold, wall thickness transition or cooling design may limit the process window. The continued pressure on the platform alone is often of limited effect in the case of shrinking water, which cannot be passed through frozen thin-walled areas to thick-wall positions. At this point, the location, size or product structure of the watering needs to be assessed.
Silver threads and gas stripes distinguish between moisture, air, volatilizers and the appearance of spray. When the inhaling material is dry, the silver silk tends to spread in the direction of the flow, accompanied by a decrease in materiality; when there is a lack of gas or back pressure for the material, the gas strip may appear at the same time as the measurement of fluctuations; and when the temperature is too high, it is too long or pollution from the respirator may release volatiles. Sometimes the appearance can be changed temporarily by increasing back pressure or lowering speed, but problems can be repeated if the water is not reached. Dryer spot, back wind filtration, pipe seal and dry transport time should be checked.
The actual diagnosis can be based on fixed other conditions, a single factor at a time and the expected results for each adjustment. For example, it is suspected that the pressure peaks will drop in parallel with the flyside before the switch is made; it is suspected that the exhaust speed will be reduced and the exhaust trough will be cleaned; and it is suspected that the reverse ring will be stopped and a double-jet or weight stability test will be performed. If defects occur after the equipment has been in operation for a certain period of time, they are also checked for smelting stops, screw wear and heat balance changes. The switchboard records should retain defective photographs, changes in parameters and validation findings to form reusable fault trees rather than leaving only final parameters.