
Toys plating screws: mix even and material compatible
Release time:2025-08-07
The Toy Plug Snail Program? Toy retrofits need to match both plastic properties, retrofitting specifications and product quality targets, and to confirm temperature rise, measurement, mixing and wear and tear performance through test modelling data. This paper combines information on star-friend screw stations to organize selection, process and validation elements.
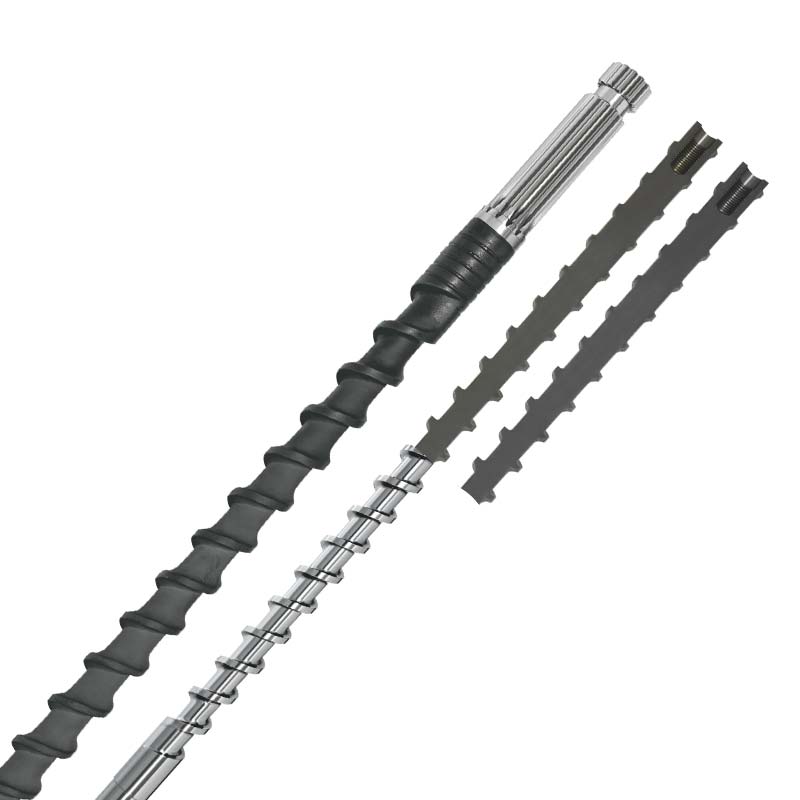
The core conclusion of the toy-skin screw.
Toy retrofits need to match both plastic properties, retrofitting specifications and product quality targets, and to confirm temperature rise, measurement, mixing and wear and tear performance through test modelling data.
Note plastic toy formation optimization: medium cut high-compatibility plume
In the field of plastic toy production, ABS and PP-based products are extremely demanding in terms of colour performance and surface quality. Such products require not only a balanced colour (colour difference E2.0), but also a smooth surface (coarse radio 0.8 m) to avoid the appearance damage caused by viscera. At present, waste rates due to mixed, rough surfaces, viscosy, etc. tend to be as high as 18 per cent when commonly used equipment is produced, and more than 60 per cent of them are mixed, which seriously affects production efficiency and product competitiveness. This paper will analyse the processing properties of ABS and PP materials in the context of specific data, and describe how the color and taste of the apostilles can be improved by increasing the colour and surface roughness of the apostilles. Special plysing screws, medium shearing, good mix structure, compatibility, high-profile solution to production pains.
Core mass pain points and technology needs for plastic toy production
Three major quality pain points for pyrotechnic toys are closely related to material performance and processing. According to industry standards, a child ' s toy must have a rough surface of 0.8 μm to avoid skin scratching; a colour difference E for a mixed product must be contained within 1.5 and no visible colour bands should be present; and the appearance of damage due to viscera must be 1 %.
The mechanisms behind these pains are different: ABS materials consist of triutron acrylene, butadiene and styrene co-polymers, with local colour deviations if they are not evenly mixed, with an average of only 70 per cent of the cochrome of the ordinary acoustic screws, which is difficult to meet; PP crystals are fast and the temperature of the molten temperature is above ± 3 °C leads to uneven surface crystals, which form rough textures (Ra≥1.2 μm); the problem is aggravated by the presence of unmelted particles in the molten body due to incomplete plasticization of the aluminum screw, or by the lack of design for the emulsion slope, which tends to fluctuate by ±8 per cent.
Technical advantages of cutting high-compatibility plume
To meet the processing needs of ABS and PP materials, the specialized retrofit screws achieved three structural breakthroughs:
It's a good mix.
The middle part of the screw sets the staggered condensing ring and barrier-like diversion structure, which is controlled at 0.6-0.9 mm and 40% less than the normal cortex, and allows for a strong radial mixing of the molten. Test data indicate that the structure increased the spread of ABS-coloured mothers to 93 per cent (or 70 per cent of the normal screw) and reduced the waste rate from 11 per cent to 2.3 per cent due to the unevenness of the mix. At the same time, the length of the amalgamation segment was increased by 20 per cent to ensure that the mixing time of the PP with the colored mother was extended to 8 seconds (5 seconds for the normal screw) and the incidence of the ribbon was reduced from 8 per cent to 1.1 per cent.
Medium shear control to improve surface smoothness degrees
Using a medium compression ratio of 2.8-3.2, the snail depth is 18% deeper than the normal screw, which stabilizes the cut rate at 100-150s-1 (the normal screw is 180-250s-1). Tests of PP materials indicate that a moderate cut-off reduces the break-up of the molecular chain, the temperature of the molten body is controlled at > 1.5 °C and the surface roughness is reduced from Ra1.2 μm to 0.6 μm to meet high industry standards. For ABS materials, a moderate cut-off avoids excessive fragmentation of the rubber phase and increases the impact intensity to 95 per cent (85 per cent after normal screw processing).
High compatibility and cleaner design, adapted to frequent material changes
The screws use 38CrMoAl materials and are nitrogenized (surface hard HV950) to accommodate a variety of materials such as ABS, PP and PE. Its unique "Line Snail + Large Guide" design reduces the amount of residue clean-up by 70 per cent during refuelling and the time of clean-up from 30 minutes to 8 minutes of normal screws. The cross-contamination rate of 0.5 per cent after the continuous replacement of five colours meets the demand for frequent changes in the toy industry.
Synergy to optimize the coordination process
Production stability was further enhanced by the process optimization of special plating screws:
Temperature control: The temperature accuracy of the drums ± 1 °C, with ABS processing temperature stable at 220 °C and PP processing temperature stable at 190 °C, avoiding mixing and surface problems due to temperature deviations.
Demolition assistance: the pressure pressure is accurately controlled by a screw (floating ≤±2bar), reduces the bonding of the molten to the mold and reduces the sticky rate from 5% to 0.8%.
Validation of effects in practical application
Production data from a toy manufacturer show an increase in product eligibility from 82 per cent to 98.6 per cent in the use of medium cut-in-compatible plastic screws. In particular, the waste rate due to the unevenness of the mix fell from 11 per cent to 2.1 per cent, the surface roughness rate from 5 per cent to 0.9 per cent, the break rate due to the viscosity from 2 per cent to 0.3 per cent; the ABS toy color differential E stabilized at 1.2-1.5, and the pP toy surface roughness Ra≤0.6 m met the high end toy standard.
In terms of cost-effectiveness, the use of materials increased from 80 per cent to 96 per cent, saving raw material costs of approximately $3.8 million per year in terms of production of 5 million toys per year; reduced fuel exchange times resulted in a 30 per cent increase in production efficiency and a 15 per cent reduction in combined production costs.
Middle-cut, high-compatibility plating screws address the root problems of the plating toy mix, rough surfaces, and viscos by optimizing the mix structure, controlling the shearing strength and increasing material compatibility. As the demand for colour diversity, safety, etc. in the toy market increases, the professional solution will become the core of the enterprise ' s efficiency-enhancing options and drive the industry towards precision production.
Data to be recorded before implementation
- Material integrity number, filling ratio, flame-retarding system, refill ratio and dry condition.
- Note plastics brand, model, screw diameter, voltage, back pressure, turn speed and current screw structure.
- Indicators of product size, wall thickness, appearance or strength, and current adverse phenomena and frequency of occurrence.
- Continuous production cycle, refuelling frequency, machine clean-up method, wear and tear record and planned useful life.
How to validate the adjustment results
It is recommended that the current process baseline be established, followed by a single-variant test model. Each round records the measurement of time, melting temperature, product weight, formation cycle and bad rate, avoiding multiple parameters being changed at the same time to determine the cause. The parameters in the text are used to illustrate design thinking and should not replace material supplier data and on-site safety protocols.
What kind of support is a star-friend screw?
The Starfleet Mechanical Equipment Co. Ltd. (Starfeng) can provide materials and situational assessments, screw structure recommendations, base and surface treatment options, non-spectrometric customization and trial modelling issues around toy acupuncture screws. The submission of information on raw materials, equipment and products could lead to more targeted programmes.
Ask for customized screws immediately, or check firstNote plastic screw productwithNote Plastic SolutionsI don't know.