
PLA/PHA Biomaterials retrofit spiral programme: low shearing and temperature control
Release time:2025-08-07
PLA/PHA biomaterials retrofit screws? The retrofitting screws of biological materials need to match both the plastic properties, the specifications of the retrospectors and the product quality targets, and to confirm the warming, measuring, mixing and wear performance through test modelling data. This paper combines information on star-friend screw stations to organize selection, process and validation elements.
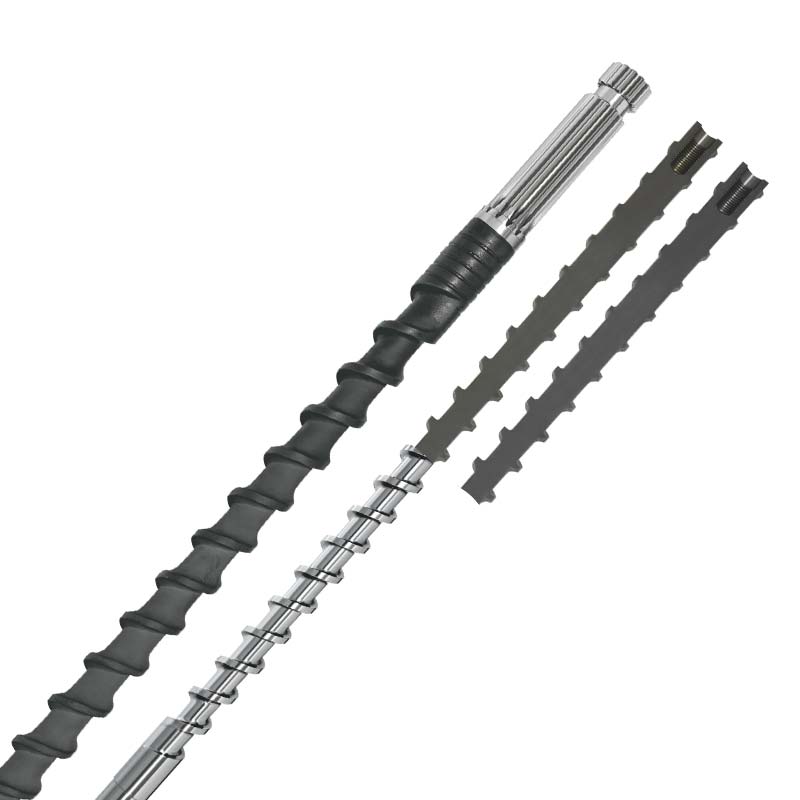
The core conclusion of biomaterials in plastic screws.
The retrofitting screws of biological materials need to match both the plastic properties, the specifications of the retrospectors and the product quality targets, and to confirm the warming, measuring, mixing and wear performance through test modelling data.
Stable pathways for the formation of environmentally friendly biological materials: low-cut, precise temperature-controlled accelerator solutions
Biodegradable materials such as PLA and PHA require strict processing conditions: a temperature window of 170-200°C and a cut-off rate of 50-100s-1. General equipment resulted in a pass rate of less than 60 per cent, with 50 per cent of the deficiencies arising from material breakdown and 25 per cent from screw residues. Low shearing, precision temperature control, and special retrofit screws for residual protection have effectively addressed these problems.
Core pain.
Decomposition: PLA lost 30 per cent of molecular weight above 210°C; PHA hydrolyzed 15 per cent over 5 minutes.
Instability: PLA viscosity changes by 20% at ±3°C; normal screws have ±5°C accuracy.
Residues: 25 per cent of products will have black dots due to the rough surface of the screw (Ra0.8 mm).
Special screw technology advantage
Low shear design: compression is 1.6-2.0, a 30 per cent increase in the snail depth and a cut rate of 60-80s-1 (1/3 of a normal screw). PLA breakdown decreased from 35 per cent to 4.2 per cent; PHA hydrolysis decreased from 15 per cent to 2.1 per cent.
Precision temperature control: ± 0.5 °C accuracy (normal ± 5 °C), stabilization of PLA viscosity fluctuates between ± 20% and ± 3%.
Residual protection mirror treatment: Ra 0.02 m + PTFE coating reduces residues by 90% and black dots from 25% to 1.3%.
316L stainless steel: five times corrosive, acid hydrolysis appropriate for PHA.
Result
PLA eligibility rate: 58 per cent →98.3 per cent; breakdown deficiency 35 per cent →3.8 per cent.
PHA medical products: PDI 2.8 →1.8; biocompatibility conformity rate 75 % 100%.
Cost savings: 4.2 million yuan/year (50 million PLA sets); efficiency gains of 40 per cent.
The screw ensures stable processing of environmentally sound biological materials and promotes biodegradable industries.
Data to be recorded before implementation
- Material integrity number, filling ratio, flame-retarding system, refill ratio and dry condition.
- Note plastics brand, model, screw diameter, voltage, back pressure, turn speed and current screw structure.
- Indicators of product size, wall thickness, appearance or strength, and current adverse phenomena and frequency of occurrence.
- Continuous production cycle, refuelling frequency, machine clean-up method, wear and tear record and planned useful life.
How to validate the adjustment results
It is recommended that the current process baseline be established, followed by a single-variant test model. Each round records the measurement of time, melting temperature, product weight, formation cycle and bad rate, avoiding multiple parameters being changed at the same time to determine the cause. The parameters in the text are used to illustrate design thinking and should not replace material supplier data and on-site safety protocols.
What kind of support is a star-friend screw?
The Starfleet Mechanical Equipment Co. Ltd. (Starfeng) provides a reset of materials and work evaluation, screw structure, base and surface treatment options, non-spectrum customization and trial modelling issues around biomaterials. The submission of information on raw materials, equipment and products could lead to more targeted programmes.
Ask for customized screws immediately, or check firstNote plastic screw productwithNote Plastic SolutionsI don't know.