
Why is a long long-duration compared to a screw for full plasticization?
Release time:2026-09-20
Increased effective length can provide additional distances for preheating, compression, melting and amalgamation, facilitating the smoothing of pressures. The working principles, selection conditions, common risk and validation methods explain why long-wire-to-heavy screws contribute to full plasticization, help retrofitting plants to stabilize plasticization and reduce the full-life cost of a screw drum.
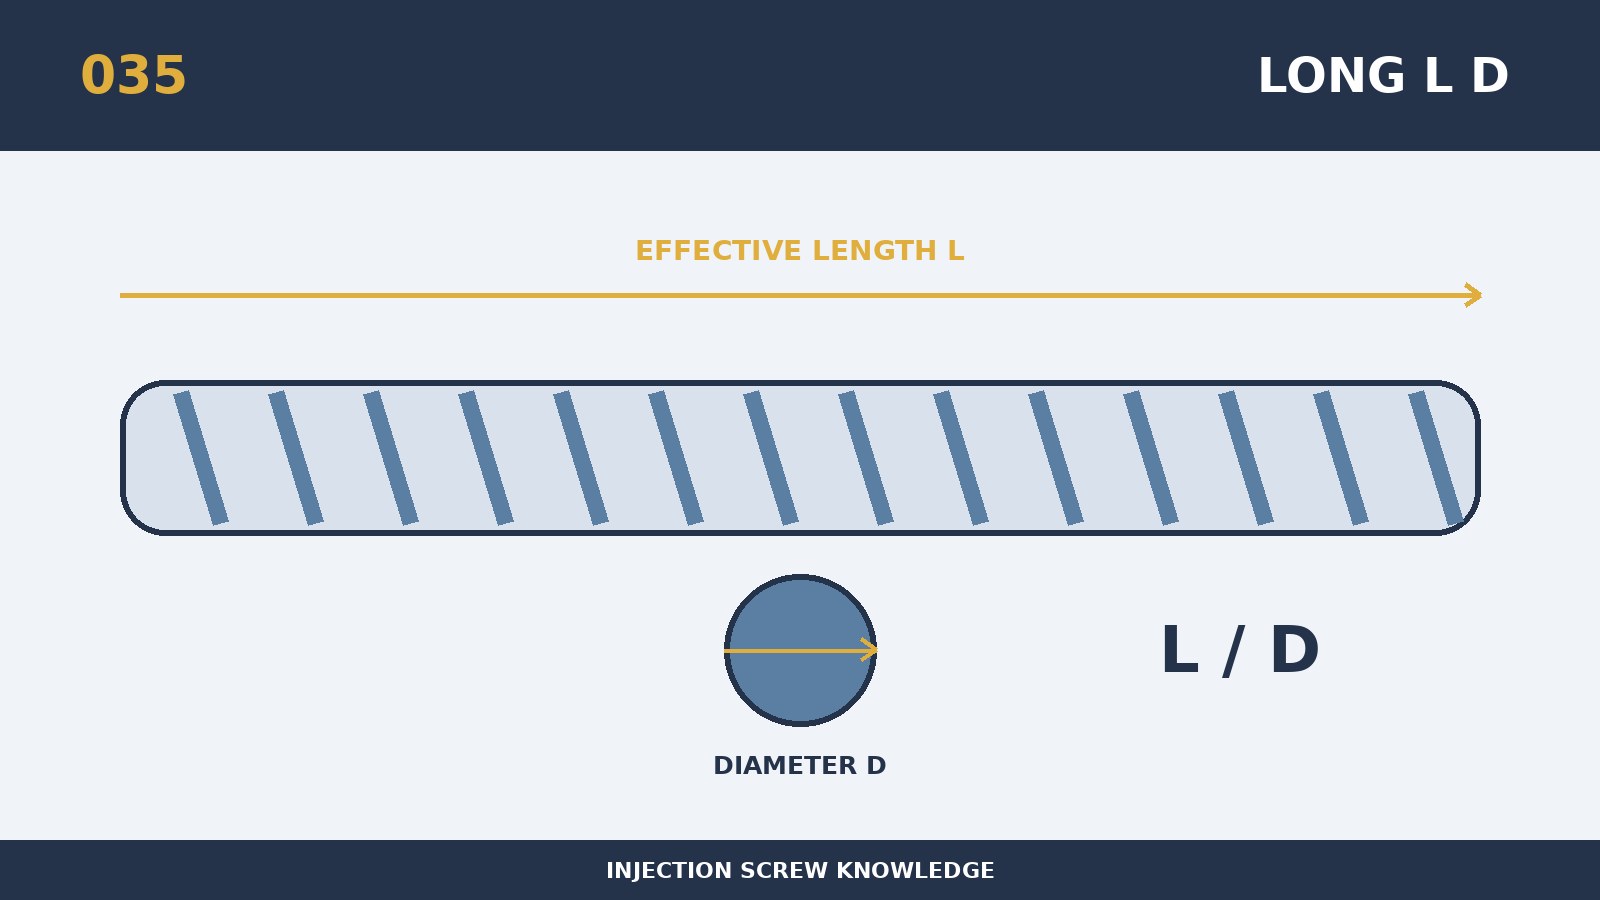
The reason why long long-range versus screws contribute to full plasticization is directly related to plasticization quality and equipment loads, and therefore design, procurement, switch and maintenance personnel should use the same set of evaluation criteria. At its core, increasing the effective length can provide additional distances for preheating, compressing, melting and mixing, and facilitate the smoothing of pressure. Long L/D does not automatically equal high quality, and its value depends on the distribution of functional segments and material stopover control. The long-range ratio is only a geometric entry, and what really determines is the effective length, distribution of the functional segments, actual production and material heat history. Parameter decision-making can be based on a failure push: short-shot, black spot, product fluctuations and overloading are listed first, and then the geometrics are identified to block the failure chain. Nominal specifications are therefore only the starting point, and the final conclusions must serve the actual resin, product and volume rhythm.
When customizing around "Why Long Long Radius vs. Snails for Full Plasticization", first collects the size of the equipment model, the original screw and the material drum, the driving power, the resin number and filling system, the sum of the single simulator, the cycle and existing defects. The specific selection principles of the topic are that engineering plastics, high-yielding or dispersal-required scenarios can assess the longer structure, with the simultaneous installation of space on a nuclear platform. The high-yield project should also reconcile the heat load of the speed-reducing box with the electric power to avoid a long-term overload of the propeller itself. The technical agreement should include quantifiable provisions for size benchmarks, key communications, material status and acceptance methods so that new, old and subsequent restorations can be compared under the same criteria.
The most important defence against the failure of the subject is that excessive length increases the length of stay, reverses deformation, creates difficulties and cleans up the burden, with a particular care to be taken in the case of heat-sensitive materials. When the size is still satisfactory and performance is abnormal, the same axiality, roughness of the surface, partial loss of coatings and thermal deformation are also examined and not only the outer diameter. For on-site processing, only one main variable is changed each time and the measurement time, twist, melting temperature, mat, injection pressure and product weight are aligned to the same pattern. If production is to be sustained by excessive temperature, turn speed or back pressure, the use of parameters to mask structures, wear or collage should be discontinued.
This replicable approach can be used to verify “why a long long- long-range compared to a screw is good for full plasticization” by comparing melting temperature differences, twists, colour change times and degradation signs at different yields to confirm the effectiveness of the new length. The screws, drums and reversible rings are proposed as side acceptances, since single-sizes do not represent a suitable axis of the combination gap with the heat. Inquiries to suppliers should also be accompanied by information on resins and fillings, risk of flame retardation or corrosion, total weight of products and fluids, photographs of available screws and equipment curves. The programme is considered to have a stable engineering value when the detection data, the good product rate, the timing of the switch and the unit cost of the eligible goods are improved.